
Why Pharmaceutical Packaging Moulds Must Match Filling and Closure Systems
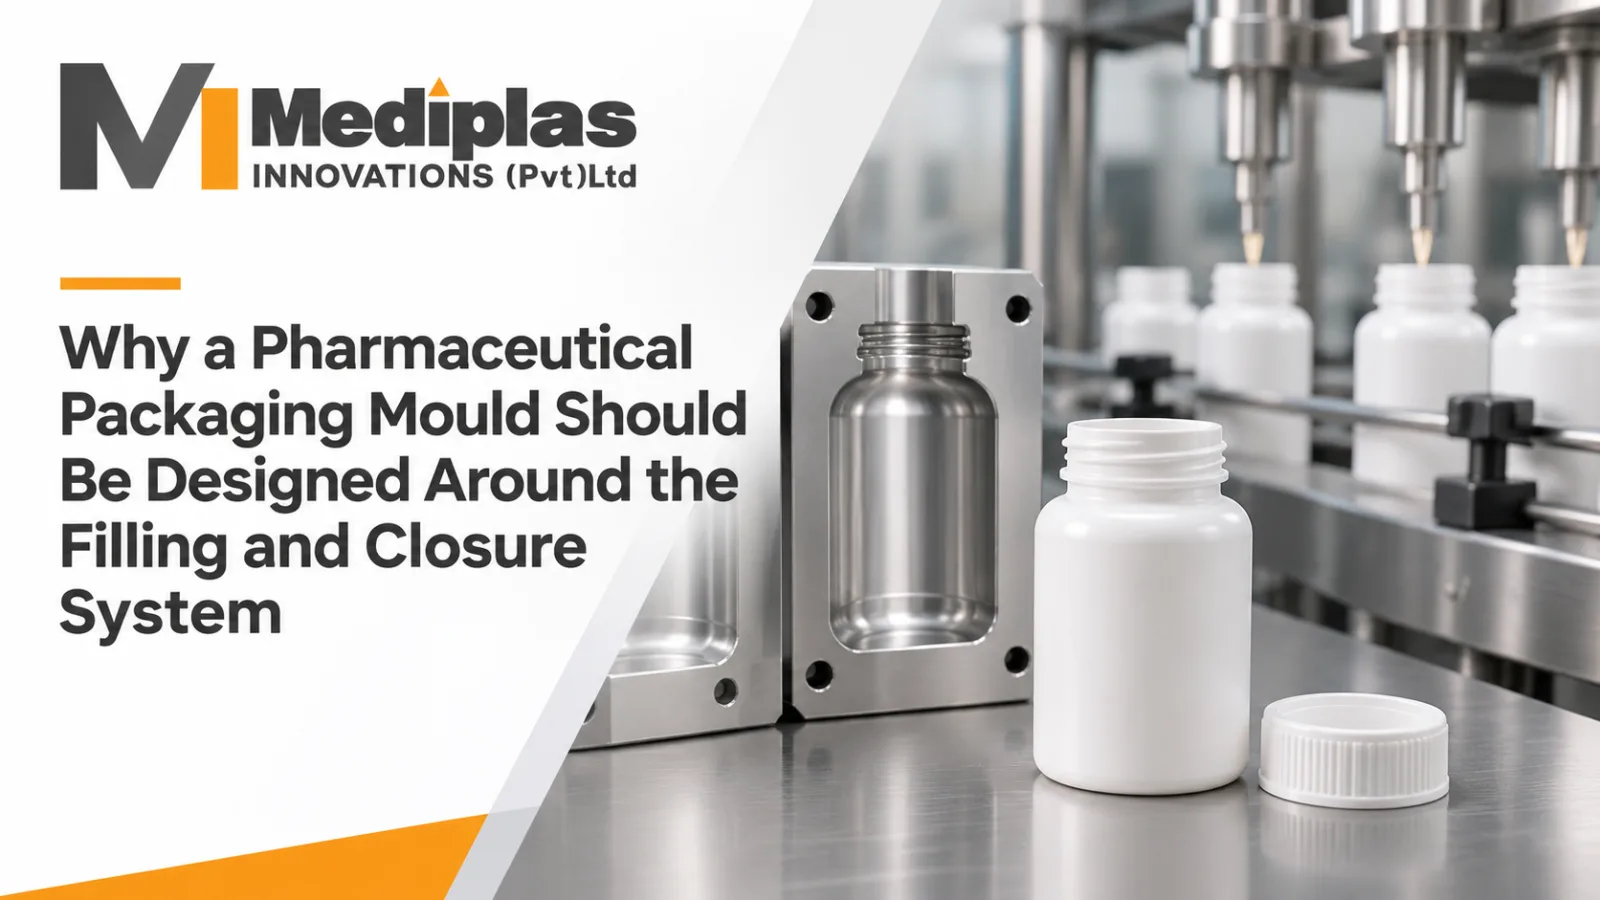
But a packaging component does not operate alone.
A bottle has to move through the filling line. A closure needs to engage with the neck. A container may need sealing, labelling, and secondary packaging. Small component changes can therefore influence equipment and processes far beyond the mould itself.
This is why pharmaceutical packaging mould design should be developed around the complete packaging and production system.
Understanding Pharmaceutical Packaging Mould Design Requirements
The Mould Produces a Component — The Factory Uses a System
The mould maker may manufacture only one bottle or cap, but the pharmaceutical plant has to combine that component with:
- The product
- Filling equipment
- Closure
- Capping equipment
- Liner or sealing system where required
- Label
- Secondary packaging
Bottle Geometry Can Affect Filling
The bottle opening, shoulder, overall height, and base can influence how the container behaves on a filling line.
Before cutting the production mould, buyers should confirm:
Filler access
Container stability
Neck handling
Conveyor clearance
Filling head compatibility
Base Stability Should Not Be an Afterthought
A bottle that stands perfectly during manual inspection may behave differently on a moving conveyor.
High or uneven centres of gravity can make some container geometries harder to handle automatically.
Design Bottle Necks and Caps Around Closure Compatibility
Neck Finish Should Be Designed From the Closure
The bottle neck and cap are two halves of one packaging interface.
Before finalising tooling, confirm:
Neck diameter
Thread geometry
Sealing surface
Cap dimensions
Application method
Any liner or seal arrangement
Do Not Develop the Bottle First and Find the Cap Later
This approach can lead to mould modifications once a closure is finally selected.
Selecting the closure early reduces avoidable redesign.
Cap Tooling Should Also Be Based on the Bottle Neck
The same principle works in reverse.
A cap mould should not be manufactured without understanding the production-intent bottle neck it needs to fit.
Closure Application Equipment Matters
The final closure geometry may influence:
Cap feeding
Orientation
Chuck or capping-head compatibility
Application torque
Line speed
Consider Induction Sealing and Dosing Component Requirements
Induction Sealing Adds Another Interface
Where induction sealing is used, the project needs to consider:
Bottle Mouth + Closure + Liner/Wadding + Capping + Induction Equipment
Tooling dimensions can affect several parts of that chain.
Dosing Components Also Need Packaging-System Context
If a mould produces a dosing cup, dropper, insert, or other pharmaceutical component, the tool should reflect the component's actual interface with the pack.
Critical Dimensions Should Be Defined by Function
Rather than applying extremely tight tolerances everywhere, determine which dimensions affect:
Filling
Closure fit
Sealing
Assembly
Label placement
Another critical packaging function
Include Filling, Labelling, and Packaging in Mould Design
Design for Manufacturing Should Include Design for Filling
A component can be easy to mould but difficult to fill or assemble.
The design review should therefore consider both manufacturing and downstream use.
Label and Decoration Areas Can Affect Bottle Geometry
If the bottle requires a pressure-sensitive label, screen print, or another decoration, the mould should provide a suitable surface.
Deep ribs and complex curvature can reduce usable decoration area.
Secondary Packaging Can Influence Dimensions
Container diameter and height determine how efficiently products fit into:
Cartons
Trays
Cases
Pallets
This is another reason the mould should not be designed from the bottle drawing alone.
Plan Pharmaceutical Packaging Tooling for Production Volume
Production Volume Should Influence Tool Configuration
A pharmaceutical pack used for a smaller product launch may need a different cavity strategy from a mature high-volume medicine.
Expected demand affects tooling economics.
More Cavities Need More Complete Validation
Where multiple cavities manufacture components simultaneously, buyers should evaluate consistency between cavities during trials.
Test Pharmaceutical Packaging Moulds Under Real Production Conditions
Trials Should Recreate the Real Packaging Workflow
Instead of inspecting an empty component on a table, trial samples should move through as much of the real process as practical:
Moulding → Inspection → Filling → Closing → Sealing Where Applicable → Labelling → Packing
Actual Production Trials Can Reveal Problems CAD Cannot
CAD models cannot fully predict every filling-line, capping, or handling interaction.
Physical trials therefore remain important before production tooling is formally approved.
Tool Modification Is Easier Before High-Volume Production
If a neck, base, or fitting feature needs adjustment, correcting it during development is generally preferable to discovering the issue after commercial inventory has already been produced.
Maintain Mould Quality and Critical Packaging Dimensions
Tool Maintenance Protects the Packaging System Too
Wear in a neck insert or another critical mould feature can gradually alter dimensions.
That may eventually appear as a capping or sealing problem rather than an obvious mould problem.
Quality Control Should Follow the Critical Interfaces
Inspection plans should focus on dimensions that influence the real package.
For example:
Neck dimensions
Bottle height
Base stability
Cap threads
Sealing areas
Component alignment
Mating features
Coordinate Packaging Mould Development With Production Equipment
Share Production Equipment Information With the Mould Manufacturer
Useful project information may include:
Filling equipment
Capping process
Line speed
Sealing method
Label equipment
Packing constraints
This helps the tooling discussion reflect the real operating environment.
The same coordination principle is important in broader turnkey pharmaceutical project planning, where equipment selection and production requirements are considered together.
A Better Pharmaceutical Tooling Sequence
Use this approach:
Product Requirement → Packaging Design → Filling & Closure Review → DFM → Mould Design → Trials → Filling-Line Test → Final Tool Approval
Working With a Pharmaceutical Packaging Mould Manufacturer
Companies evaluating a pharmaceutical packaging mould manufacturer in Pakistan should share the filling, closure, and assembly requirements alongside the component drawing before the production mould is finalised.
Final Thoughts
A mould produces one plastic component at a time, but that component eventually becomes part of a complete pharmaceutical packaging line.
The strongest tooling projects are designed backward from the final filling, closing, and packing process—not forward from an isolated CAD model.
0 comments
Log in to leave a comment.
Be the first to comment.