
What Fire Pump Considerations Matter for Connecticut Manufacturing Plants? Connecticut Manufacturing Fire Pumps
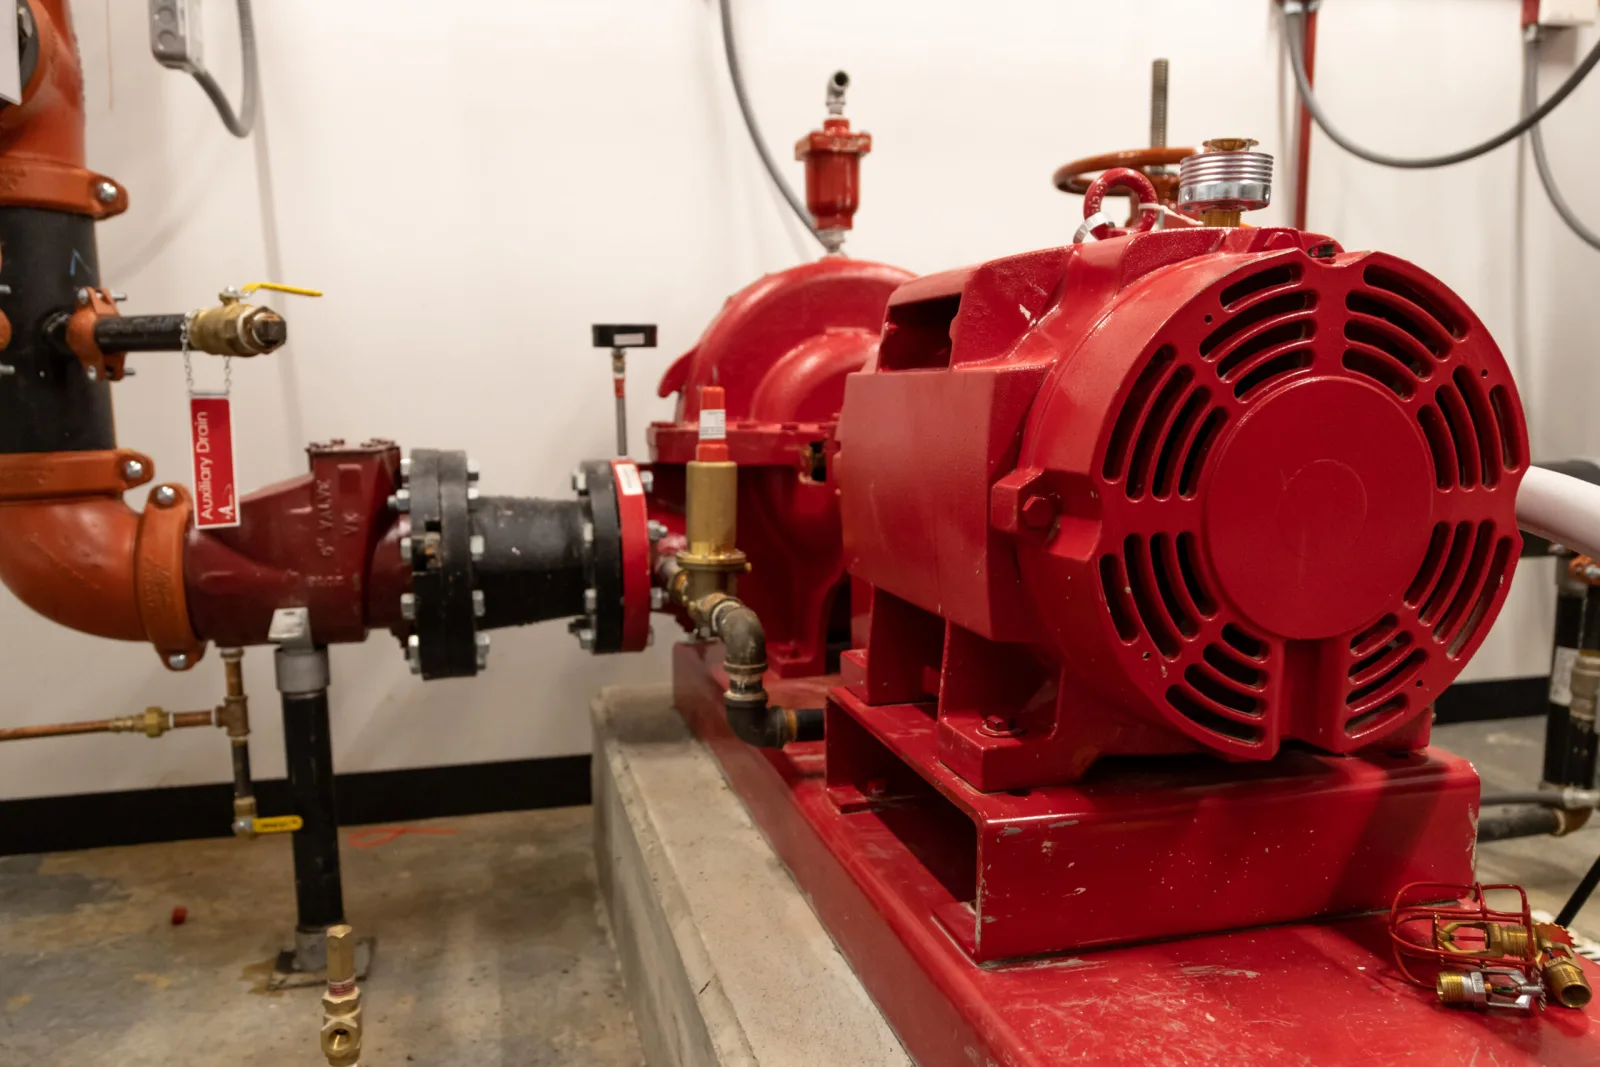
Manufacturing plants face fire protection challenges that go beyond those of typical commercial buildings. Production machinery, combustible materials, chemical storage, electrical equipment, and large warehouse areas can all influence how a fire develops and how much water a fire protection system needs. A fire pump must deliver the required water flow and pressure to support the building's sprinkler, standpipe, and other fire protection systems when the available water supply cannot meet their demands.
For facility managers, engineers, contractors, and industrial property owners, selecting the right fire pump requires a closer look at the plant's operations, water supply, building layout, and potential fire hazards. A pump that meets the needs of a small manufacturing unit may not provide adequate performance for a large industrial facility with multiple production areas and storage zones.
Understanding the key considerations behind Connecticut manufacturing fire pumps can help facility teams make informed equipment decisions, plan upgrades, and maintain reliable fire protection.
Let's examine the factors that matter when specifying fire pumps for Connecticut manufacturing plants.
Why Do Manufacturing Plants Need Specialized Fire Pump Considerations?
Manufacturing facilities often contain several different fire hazards under one roof. A plant may have production lines, electrical rooms, loading docks, raw material storage, finished goods warehouses, and areas where flammable liquids or combustible dust are present.
Each area can have different fire protection requirements.
For example, a facility that manufactures metal components may have different protection needs from a plant that processes plastics, stores packaging materials, or handles industrial chemicals. The type of materials, storage arrangement, ceiling height, and production equipment all influence the fire protection design.
Fire pumps become particularly important when the municipal water supply cannot deliver the pressure and flow required by the system.
A properly selected fire pump helps:
Deliver the required water pressure to sprinkler systems and standpipes.
Support fire protection systems across large manufacturing buildings.
Compensate for inadequate municipal water pressure.
Maintain the required hydraulic performance during a fire emergency.
Supply water to different areas of a facility when the system design calls for it.
The objective is not simply to install a higher-capacity pump. It is to select equipment that matches the building's calculated fire protection demand.
1. Evaluate the Plant's Fire Hazards and Occupancy Classification
The first consideration is understanding what happens inside the manufacturing facility.
Different manufacturing processes introduce different fire risks. For example, facilities handling flammable liquids may require a different protection strategy from those storing cardboard packaging or manufacturing plastic products.
Engineers should evaluate:
Raw materials and finished products stored inside the building.
Combustible liquids, gases, and chemicals used in production.
Electrical equipment, transformers, and machinery.
Combustible dust generated during manufacturing.
Storage heights and rack configurations.
Production areas where heat-generating processes take place.
These details help determine the applicable fire protection requirements and hydraulic demand.
The facility's occupancy classification and hazard classification should also be evaluated under the applicable building and fire codes. Sprinkler system design may depend on the hazard classification, storage arrangement, commodity type, and other building characteristics.
For instance, a plant with high-piled combustible storage may require a substantially different sprinkler design from a facility with ordinary manufacturing operations.
Why does this matter for fire pump selection?
The fire pump must support the water demand established by the fire protection system design. Choosing a pump based only on the building's square footage can lead to an unsuitable selection because two facilities of similar size may have very different fire protection requirements.
2. Check the Available Water Supply and Municipal Pressure
Before selecting a fire pump, engineers need to understand how much water the facility can receive from its existing supply.
Many manufacturing plants depend on municipal water systems. However, the available pressure and flow may not be sufficient to meet the demands of the building's fire protection systems.
Several factors can affect water availability:
Distance between the facility and the municipal water main.
Existing water main capacity and pressure.
Seasonal variations in water supply.
Simultaneous demand from nearby industrial properties.
Elevation differences across the manufacturing site.
Pressure losses through pipes, valves, and fittings.
A current water flow test is an important starting point. It provides information about available flow and residual pressure, helping engineers understand whether the existing supply can meet the calculated fire protection demand.
If the available pressure is insufficient, a fire pump may be required to increase the pressure delivered to the system.
However, the pump cannot compensate for an inadequate water source indefinitely. Its selection must account for the actual water supply conditions, including the available suction pressure and required flow.
Some facilities may also need to evaluate on-site water storage, such as dedicated fire water tanks, depending on their water supply conditions and applicable design requirements.
For Connecticut manufacturing facilities undergoing expansion, a new water supply assessment is particularly important. Additional production lines, warehouse space, or sprinkler coverage can change the building's overall fire protection demand.
3. Calculate the Required Fire Pump Flow and Pressure
Flow and pressure are two of the most important factors in fire pump selection.
A fire pump must provide enough water to meet the hydraulic requirements of the connected fire protection systems. Selecting a pump with insufficient capacity can compromise system performance, while an unnecessarily oversized pump can introduce additional design and operational complications.
Engineers generally evaluate two primary measurements:
Flow rate: The amount of water the pump must deliver, typically measured in gallons per minute (GPM).
Pressure: The pressure required to move water through the fire protection network and reach the hydraulically demanding areas of the building, typically measured in pounds per square inch (PSI).
The required pump capacity depends on several factors:
Sprinkler system hydraulic calculations.
Standpipe system requirements, where applicable.
Hose stream allowances.
Building height and elevation differences.
Friction losses in the piping network.
Required pressure at the most demanding system connection.
Available suction pressure.
For example, a manufacturing plant with multiple floors and extensive sprinkler coverage may require a different pump arrangement from a single-story facility with a smaller protected area.
Engineers should use hydraulic calculations to establish the required operating point rather than selecting a pump based on a general industrial capacity recommendation.
The selected pump's certified performance curve should also be reviewed to confirm that it can meet the required operating conditions.
4. Choose the Right Fire Pump Type and Driver
Manufacturing plants have different operational requirements, which makes fire pump type and driver selection an important part of the design process.
Common fire pump configurations include horizontal split-case, vertical turbine, and end-suction pumps. The appropriate option depends on the water source, available installation space, required capacity, and system design.
Horizontal Split-Case Fire Pumps
Horizontal split-case pumps are widely used in industrial fire protection applications. Their design allows access to internal components for inspection and maintenance.
They can be suitable for manufacturing plants requiring substantial water flow, provided the available suction conditions and installation arrangement meet the pump's requirements.
Vertical Turbine Fire Pumps
Vertical turbine pumps are commonly considered when the water source is located below the pump, such as in a dedicated underground water tank or another suitable water source.
They can be useful where a conventional horizontal pump arrangement cannot achieve the required suction conditions.
End-Suction Fire Pumps
End-suction pumps offer a relatively compact arrangement. They may be appropriate for smaller manufacturing facilities or applications where the required flow and pressure fall within the pump's certified performance range.
The pump configuration is only one part of the decision. The driver also matters.
Electric motor-driven fire pumps
Electric-driven pumps are often considered where a dependable electrical supply is available. Engineers must evaluate the power source, motor requirements, controller arrangement, and applicable electrical protection provisions.
Diesel engine-driven fire pumps
Diesel-driven pumps can provide an alternative where an appropriate electric power supply is unavailable or where the fire protection design calls for a separate engine-driven arrangement. Their selection requires consideration of fuel storage, ventilation, exhaust arrangements, cooling, and battery reliability.
For manufacturing plants, the final choice should reflect site conditions, reliability objectives, applicable codes, and the requirements established by the fire protection engineer.
5. Consider the 2025 NFPA 20 Requirements
Fire pump selection and installation should follow the applicable edition of NFPA 20, Standard for the Installation of Stationary Pumps for Fire Protection, together with the codes adopted by the local jurisdiction.
The 2025 edition of NFPA 20 introduces several noteworthy changes that make it relevant to current fire pump specifications.
These include:
Expanded provisions for automatic and remote automatic testing of electric-driven fire pumps.
New requirements addressing automatic and remote automatic testing of diesel-driven fire pumps.
Clarifications concerning fire pump controllers and automatic transfer switches.
Additional provisions addressing alternate power sources for certain electrically powered diesel pump room components.
Clarifications involving pressure relief valves, sprinkler protection, and overcurrent protection.
These developments highlight the importance of considering testing capabilities, controller arrangements, and power reliability during equipment selection rather than treating them as afterthoughts.
For Connecticut projects, there is an important code-adoption distinction. As of October 30, 2026, Connecticut's Department of Administrative Services reports that the next state building and fire codes have been delayed pending approval. The 2022 Connecticut codes therefore remain the published adopted baseline on the state's code-adoption information. The 2025 NFPA 20 edition should not automatically be treated as the locally adopted edition for every project. Engineers should confirm the applicable requirements with the local authority having jurisdiction (AHJ).
CT.gov+26. Evaluate the Fire Pump Room and Installation Environment
A manufacturing plant's fire pump room must provide suitable conditions for the equipment to operate reliably.
Industrial facilities can expose mechanical and electrical equipment to dust, moisture, vibration, temperature fluctuations, and other environmental conditions. These factors should be considered when planning the pump room.
Important considerations include:
Accessibility: The room should provide adequate clearance for inspection, testing, component replacement, and maintenance activities.
Ventilation: Diesel-driven fire pumps require appropriate ventilation and provisions for engine combustion air and heat removal.
Temperature control: The room should maintain suitable temperatures to protect equipment and prevent freezing, particularly during Connecticut winters.
Drainage: Proper drainage helps prevent water accumulation around the pump, motor, controller, and other equipment.
Flood protection: The location should be evaluated for potential flooding and water intrusion that could affect equipment availability.
Lighting and access: Personnel should be able to reach the equipment safely and identify controls and indicators during inspections and emergencies.
The fire pump room should also be protected and arranged in accordance with applicable NFPA 20 provisions and local code requirements.
For manufacturing plants with limited floor space, room planning deserves attention early in the project. Trying to accommodate a large fire pump assembly after the building layout has been finalized can create unnecessary design complications.
7. Account for Connecticut's Climate and Seasonal Conditions
Connecticut's seasonal temperature changes introduce additional considerations for industrial fire protection equipment.
Winter temperatures can affect water-filled piping, exposed equipment, fuel systems, batteries, and other components if they are not properly protected.
Fire pump installations should be evaluated for:
Adequate heating and freeze protection.
Protection of exposed water supply piping.
Suitable insulation where required.
Reliable diesel engine starting batteries.
Proper storage and handling of diesel fuel.
Protection against moisture and condensation.
Drainage around outdoor equipment and water supply connections.
A fire pump that operates reliably during warmer months must also remain ready during freezing conditions.
This is particularly important for manufacturing facilities that operate continuously or have limited personnel available outside normal business hours.
8. Assess Power Supply and Backup Arrangements
Electrical reliability is another important consideration for manufacturing facilities.
Production plants may experience electrical disturbances, planned shutdowns, equipment upgrades, or changes in their power distribution systems. Fire protection equipment must be considered separately from ordinary production loads.
When specifying an electric motor-driven fire pump, engineers should review:
Available voltage and electrical service capacity.
Motor starting characteristics.
Electrical feeder arrangements.
Controller requirements.
Automatic transfer switch provisions, where applicable.
The reliability of the power source.
Applicable emergency and standby power requirements.
A diesel-driven pump may be considered where the project requires an alternative driver arrangement.
However, the choice between electric and diesel operation should not be based on assumptions that one is universally more reliable. Each option has different power, fuel, maintenance, and operational requirements.
The goal is to establish a fire pump arrangement that can operate under the conditions anticipated by the fire protection design.
9. Plan for Inspection, Testing, and Maintenance
Selecting the right fire pump is only the beginning. Regular inspection, testing, and maintenance are essential to keep the system ready for an emergency.
Manufacturing facilities often operate around the clock, making it important to establish a maintenance schedule that does not interfere unnecessarily with production activities.
NFPA 25 provides the framework for inspection, testing, and maintenance of water-based fire protection systems. Its current published edition is 2026, although facilities must follow the edition adopted by their jurisdiction and any applicable local requirements.
NFPA+1Fire pump maintenance planning should cover several areas.
Weekly or periodic operational checks: Check the pump room environment, controller indicators, power availability, and other conditions according to the applicable inspection schedule.
Churn testing: Evaluate the pump's operation at no-flow conditions to identify potential problems with starting, operation, or system pressure.
Annual flow testing: Verify pump performance at relevant flow conditions and compare the results with the established acceptance test baseline.
Diesel engine checks: Review fuel condition, batteries, cooling arrangements, lubrication, and other engine components.
Controller inspections: Check for alarms, abnormal indicators, electrical issues, and other signs that may affect pump readiness.
Maintaining accurate records is equally important. Facility teams should document test results, maintenance activities, equipment changes, and identified deficiencies.
Comparing current performance with previous test records can help identify developing problems before they affect fire protection readiness.
10. Consider Future Production Expansion and System Modifications
Manufacturing plants rarely remain unchanged throughout their operating life. Companies may add production lines, expand warehouses, introduce new machinery, or change the materials used in manufacturing.
These modifications can affect fire protection requirements.
For example, adding high-rack storage may change sprinkler design requirements. Introducing new combustible materials can also affect the hazard classification and the water demand of the protected area.
Before making significant changes, facility owners should evaluate whether the existing fire pump can support the revised system requirements.
Important questions include:
Will the new production area increase sprinkler demand?
Will additional floors or equipment create greater pressure requirements?
Does the existing water supply provide sufficient flow?
Can the current pump operate at the revised hydraulic demand?
Will new piping introduce additional friction losses?
Does the existing pump room have enough space for equipment modifications?
An existing fire pump should never be assumed suitable for an expanded facility simply because it has been operating without problems.
Hydraulic calculations and equipment performance records should guide decisions about upgrades or replacement.
11. Review Pump Performance, Certifications, and Manufacturer Documentation
Industrial fire pump selection should involve more than comparing horsepower, price, or nominal flow ratings.
Engineers and purchasing teams should review the pump's certified performance information and supporting documentation.
Some important details include:
Rated flow and pressure.
Certified pump performance curves.
Driver specifications.
Controller compatibility.
Available suction conditions.
Applicable UL listing and FM approval requirements.
Installation and operating instructions.
Factory test documentation.
Replacement component availability.
UL listing and FM approval should be evaluated according to project specifications and applicable code requirements. They should not be assumed to be interchangeable with every other certification or approval.
Factory performance testing is also an important part of equipment evaluation. For example, Aurora fire pumps are associated with factory performance testing at 50%, 100%, and 150% of rated flow, subject to the applicable product and test requirements.
For manufacturing plants, documentation helps engineers verify that the selected equipment meets the design specifications and provides a reliable reference for future inspections and maintenance.
Common Fire Pump Selection Mistakes Manufacturing Plants Should Avoid
Even well-planned industrial projects can encounter problems when fire pump selection is based on incomplete information.
Here are some common mistakes worth avoiding:
Common mistake | Why it matters |
|---|---|
Selecting a pump based only on building size | Building area does not establish the actual hydraulic demand. |
Ignoring municipal water pressure | The pump may not receive the suction conditions required for proper operation. |
Overlooking future expansion | New production areas may increase fire protection demand. |
Choosing an unsuitable driver | Electrical or diesel arrangements may not match site conditions. |
Neglecting pump room requirements | Poor access, ventilation, or temperature control can affect equipment reliability. |
Ignoring testing requirements | Undetected performance issues can compromise system readiness. |
Overlooking equipment documentation | Missing performance information makes future evaluation more difficult. |
Avoiding these mistakes starts with a detailed understanding of the facility and its fire protection requirements.
Frequently Asked Questions
1. What Type of Fire Pump Is Suitable for a Connecticut Manufacturing Plant?
The right fire pump depends on the facility's water supply, required flow and pressure, building configuration, and fire protection design. Horizontal split-case, vertical turbine, and end-suction pumps may all be suitable for different applications.
2. How Do I Determine the Required Fire Pump Capacity for an Industrial Building?
A qualified fire protection engineer determines the required flow and pressure through hydraulic calculations. These calculations consider sprinkler demand, standpipe requirements where applicable, hose stream allowances, elevation differences, and piping friction losses.
3. Are Diesel Fire Pumps Suitable for Manufacturing Facilities?
Yes. Diesel-driven fire pumps can be suitable for manufacturing facilities, particularly where the project requires an alternative to an electric motor-driven arrangement. Fuel storage, ventilation, cooling, batteries, and engine maintenance must be considered.
4. How Often Should Manufacturing Facility Fire Pumps Be Tested?
Testing frequency depends on the applicable NFPA 25 edition, local code requirements, and the pump's configuration. Weekly inspections and testing requirements, periodic flow testing, and annual performance evaluations should be established according to the applicable standard.
5. Does Connecticut Require Fire Pumps in All Manufacturing Buildings?
No. A fire pump is not automatically required in every manufacturing building. The need depends on the building's fire protection requirements, available water supply, hydraulic calculations, and applicable building and fire codes.
Choose the Right Fire Pump for Your Connecticut Manufacturing Facility
Fire pump selection is an important part of protecting manufacturing operations, industrial equipment, stored materials, and building occupants. From evaluating water supply conditions to choosing the right pump configuration, every decision should reflect the facility's actual fire protection requirements.
For Connecticut manufacturing plants, it is equally important to consider seasonal conditions, electrical reliability, inspection requirements, and future production changes. A properly specified fire pump should meet the system's calculated hydraulic demand while aligning with applicable codes and project requirements.
Looking for fire pump equipment for an industrial project?
Callaghan Pump & Controls, Inc. supplies fire pumps and related pumping equipment for commercial and industrial applications. With more than 14 years of experience serving the New York metropolitan area, Callaghan works with established pump manufacturers, including Aurora, to help customers evaluate equipment options for their project requirements.
Explore Callaghan Pump & Controls to learn more about available fire pump solutions for manufacturing and commercial facilities.
0 comments
Log in to leave a comment.
Be the first to comment.