
Understanding Belco Tunnel Parts and Their Role in Shrink Packaging Equipment
Understanding how belco tunnel parts work, when they require replacement, and how to maintain them can help businesses preserve packaging quality and minimize unnecessary interruptions.
Shrink packaging systems help businesses prepare products for storage, transportation, and retail distribution. These machines use controlled heat to shrink packaging film around items, creating a secure and uniform finish. Conveyor belts play an important role in this process by moving packages through the heating chamber at a consistent speed. Understanding how belco tunnel parts work, when they require replacement, and how to maintain them can help businesses preserve packaging quality and minimize unnecessary interruptions.
How Tunnel Belts Support Packaging Operations
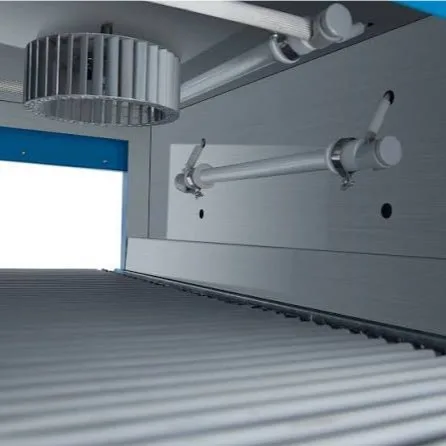
A shrink tunnel conveyor belt moves products through a heated chamber where circulating hot air causes the packaging film to contract around each item. Consistent movement allows products to receive the appropriate amount of heat without remaining in one location for too long.
When reviewing belco tunnel parts, it is important to consider how each component contributes to the machine's overall performance. The belt must work in coordination with the conveyor drive, temperature controls, airflow system, and other mechanical components. If the belt moves unevenly or slips during operation, packages may receive inconsistent heat exposure, potentially affecting their final appearance.
Common Signs of Tunnel Belt Wear
Conveyor belts experience continuous movement, friction, and exposure to elevated temperatures. Over time, these operating conditions can contribute to wear that affects performance.
Several signs may indicate that a belt requires inspection or replacement:
Uneven movement: The conveyor may hesitate, jerk, or travel inconsistently during operation.
Visible surface damage: Fraying, cracking, deformation, or other deterioration may indicate that the belt is approaching the end of its service life.
Tracking problems: A belt that repeatedly shifts toward one side may indicate alignment issues, worn components, or incorrect tension.
Inconsistent package movement: Products may tilt, shift, or travel through the heating chamber at an uneven pace.
Unusual operating sounds: Scraping, rubbing, or other unexpected noises may suggest a mechanical problem that needs investigation.
These symptoms do not always mean the belt itself is defective. Drive rollers, bearings, alignment mechanisms, and other conveyor components can produce similar problems. Examining the complete assembly helps identify the underlying cause before replacement work begins.
Choosing the Correct Replacement Belt
Selecting a replacement conveyor belt requires more than matching its general appearance. Compatibility with the specific machine model and the manufacturer's part number should be the starting point.
When evaluating belco tunnel parts, several practical considerations deserve attention. These include the belt's dimensions, material suitability, operating temperature requirements, and compatibility with the conveyor's drive and tracking arrangement. An incorrect belt can create installation difficulties, interfere with smooth movement, or wear prematurely.
Maintenance Practices That Extend Belt Life
Regular inspection helps identify developing problems before they interrupt production. The appropriate inspection frequency depends on operating hours, packaging volume, environmental conditions, and the equipment manufacturer's recommendations.
Begin by following the machine's approved shutdown and isolation procedures before inspecting conveyor components. Never reach into a moving conveyor or heated tunnel.
Once the equipment is safe to inspect, examine the belt for visible damage, contamination, and irregular wear. Check the surrounding conveyor assembly for debris, loose fasteners, damaged rollers, and signs of misalignment. Cleaning should follow the manufacturer's instructions to avoid damaging the belt material or introducing unsuitable chemicals.
Operators should also monitor conveyor movement during normal production. Recording recurring tracking problems, unusual noises, and replacement dates can reveal patterns that require corrective maintenance.
Improving Reliability Through Preventive Maintenance
Preventive maintenance is most effective when it combines routine inspections with timely repairs and accurate documentation. Keeping essential replacement components identified in advance can help maintenance teams respond more efficiently when wear becomes noticeable.
A practical maintenance plan should include inspection schedules, equipment-specific part numbers, records of previous failures, and clear procedures for reporting performance changes. Training operators to recognize early warning signs also supports faster intervention.
Maintaining suitable spare-part records for belco tunnel parts can further simplify future maintenance planning. By verifying compatibility before installation and addressing related mechanical problems, facilities can reduce repeat failures and maintain more consistent packaging operations.
Conclusion
Reliable shrink packaging depends on the coordinated performance of conveyor belts, heating systems, airflow controls, and other essential mechanical components. For equipment owners seeking reliable parts identification and assistance with replacement requirements, Machine Parts Toolbox can serve as a reference point when reviewing available machine components and confirming the details needed for a suitable replacement.
0 comments
Log in to leave a comment.
Be the first to comment.