
Twin Blade Cold Saw Applications in Tube and Pipe Manufacturing
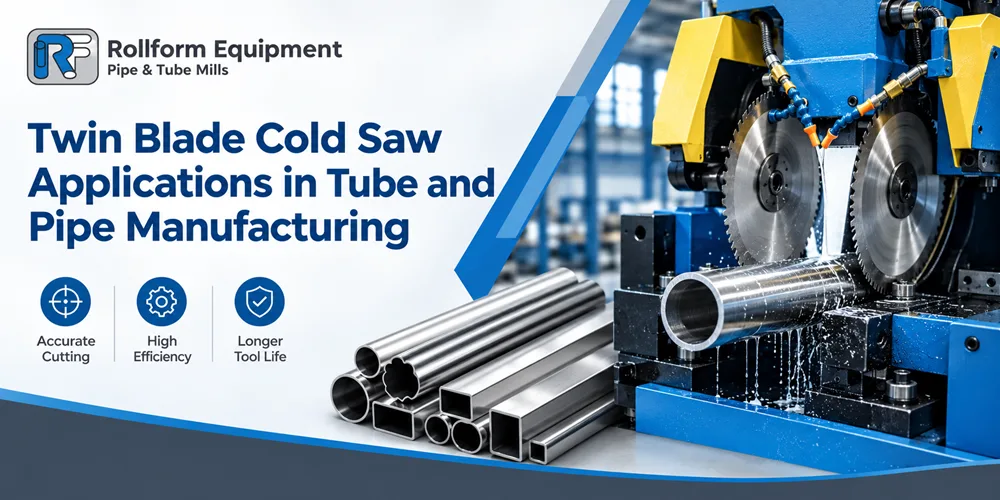
Cutting large-diameter tubes used to mean choosing between speed and finish quality. A twin blade cold saw changes that equation, and this article walks through how the technology works, what makes it efficient, and which tube and pipe applications actually benefit most.
How Twin Blade Cold Saw Technology Improves Tube and Pipe Manufacturing
Twin-blade systems bring a different cutting logic to the tube mill floor, one built around speed and edge quality together. A few core mechanisms explain why manufacturers keep switching over from older cutting methods.
● Simultaneous Twin Blade Cutting for Higher Productivity
Two blades move linearly inward from opposite sides of the tube, so the cut completes in a fraction of the time an orbital saw needs. Because both blades work together, mill speeds can climb well beyond what single-blade cutting typically allows. This is why the method suits high-output tube mills, where cycle time directly affects daily tonnage.
● Accurate Burr-Free Cutting With Better Length Control
Since the blades meet from both sides at once, the cut edge stays clean, with minimal burr formation compared with single-blade methods. At the same time, feed, speed, and RPM stay fully adjustable, so length accuracy holds even across long production runs. That level of control matters most when tubes move straight into welding, forming, or assembly without secondary finishing.
● Reduced Blade Wear for High-Volume Production
Blade life improves partly because the cutting load is shared between two edges, rather than concentrated on a single blade throughout the cycle. Operators also get the option of HSS or TCT blades, depending on the tube material and expected run length. Consequently, tooling costs stay lower over time, even under continuous high-volume operation.
Where Twin Blade Cold Saw Systems Deliver the Best Performance
Not every cutting job calls for the same setup on the mill floor. There are specific tube types, materials, and production considerations that make a twin-blade system ideal.
● Manufacturing Large-Diameter and Heavy-Wall ERW Tubes
Large-diameter and heavy-wall ERW tubes need a cutting method that keeps pace with rising mill output, and Grand View Research pegs ERW growth at a 6.3% CAGR through the forecast period. A twin blade cold saw handles that pace comfortably, since both blades share the load across thicker wall sections. As a result, producers can hold tight tolerance even as tube diameters and wall thickness increase.
● Processing Carbon Steel, Stainless Steel and High-Tensile Tubes
Carbon steel, stainless steel, and high-tensile grades each respond differently under a cutting blade, so machine settings need adjusting per material and wall thickness. A cold saw cut-off copes with this range because feed and RPM can be tuned per grade rather than fixed at one setting. This adaptability is why fabricators processing mixed material batches favour the format over rigid single-setting alternatives.
● Applications Requiring ID Bead Removal and High-Speed Cutting
ID bead removal calls for a cutting approach that avoids fully piercing the hardened, scarfed bead left after welding. A flying saw suits this task well, since its blades cut around that hardened section rather than through it, extending blade life considerably. Combined with high mill speeds, this makes the format a practical fit for continuous ERW production lines.
0 comments
Log in to leave a comment.
Be the first to comment.