
Trace Moisture: Importance of Accurate Moisture Monitoring in Industrial Applications
Moisture control is an essential requirement in industries where gas purity, product quality, and equipment performance must be maintained. Even very small quantities of water vapor can create problems in sensitive industrial processes. Excess moisture may contribute to corrosion, contamination, unwanted chemical reactions, and damage to expensive equipment. Industries that work with specialty gases, compressed air, pharmaceuticals, and chemical products need reliable methods to identify and control moisture levels. Advanced measurement technologies make it possible to detect small amounts of water vapor and maintain suitable operating conditions. Accurate monitoring also helps businesses improve production consistency, reduce maintenance problems, and protect sensitive equipment. Understanding moisture detection methods and their industrial applications can help businesses make better decisions about their measurement requirements.
What Is Trace Moisture and Why Does It Matter?
Trace moisture refers to very small quantities of water vapor present in air, gases, or other materials. These moisture levels are often too low to be identified through ordinary humidity measurements, making specialized detection instruments necessary.
In industrial environments, controlling even small amounts of moisture can be important. For example, specialty gas manufacturers require carefully controlled moisture levels to maintain gas purity. Similarly, semiconductor production facilities use highly controlled environments where unwanted water vapor may affect sensitive manufacturing processes.
Moisture can also create problems in compressed air systems. When water vapor accumulates and condenses inside pipelines, it may cause corrosion, damage pneumatic components, and reduce equipment efficiency.
Monitoring small moisture concentrations helps operators understand the condition of their systems and take corrective action when necessary. This makes accurate measurement an important part of industrial quality control and preventive maintenance.
How Is Trace Moisture Measured?
Measuring very low moisture concentrations requires specialized instruments that can detect small changes in water vapor levels. Different technologies are used depending on the gas composition, required sensitivity, and operating conditions.
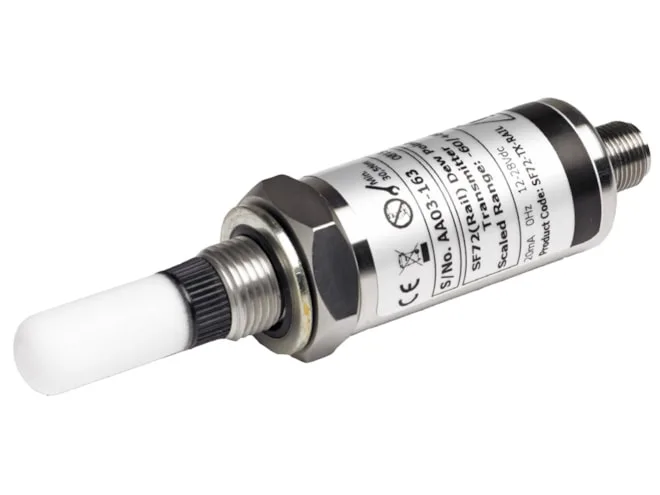
Aluminum oxide sensors are commonly used for low-moisture applications. They detect changes in electrical properties as water vapor interacts with the sensing material. The instrument processes these changes and calculates the moisture concentration or corresponding dew point.
Chilled mirror technology uses a different approach. It cools a reflective surface until condensation begins to form. The temperature at which this occurs provides a measurement of the dew point.
Other advanced sensing technologies are also available for applications requiring specific measurement ranges and high sensitivity.
Measurement results may be displayed in parts per million (ppm), parts per billion (ppb), or dew point temperature. The appropriate unit depends on the industrial process and measurement requirements.
Importance of Moisture Control in Industrial Gas Systems
Industrial gases are widely used in manufacturing, chemical processing, electronics production, and other specialized applications. Their quality can directly affect production performance and the reliability of finished products.
Unwanted water vapor may change gas properties, interfere with chemical reactions, or create condensation in pipelines and storage equipment. This can lead to operational problems and increase maintenance requirements.
In natural gas processing, moisture monitoring helps operators evaluate gas quality and reduce the risk of condensation-related problems. In specialty gas production, accurate measurements support product purity and quality assurance.
Semiconductor manufacturing also requires extremely controlled gas conditions. Even small amounts of moisture may affect sensitive production processes, making reliable measurement particularly important.
Proper moisture control helps industries maintain suitable gas conditions and reduce the possibility of unexpected process interruptions.
Common Industrial Applications of Trace Moisture Monitoring
Different industries use specialized moisture measurement equipment according to their operational requirements.
Natural Gas Processing: Monitoring moisture helps evaluate gas quality and identify conditions that may contribute to condensation or hydrate formation in pipelines.
Semiconductor Manufacturing: Highly controlled production environments require monitoring of moisture in specialty gases to protect sensitive electronic components.
Pharmaceutical Industry: Certain manufacturing and packaging processes require controlled moisture conditions to protect ingredients and maintain product stability.
Chemical Processing: Moisture measurement helps maintain suitable gas conditions and supports processes where water vapor may influence chemical reactions.
Power Generation: Monitoring moisture in industrial gas systems helps protect equipment and maintain reliable operating conditions.
Industrial Gas Production: Manufacturers use specialized analyzers to verify gas purity and maintain required moisture specifications.
Benefits of Using Advanced Moisture Analyzers
Modern moisture analyzers provide several advantages for industries that require precise monitoring. One major benefit is their ability to detect extremely low water vapor concentrations. This makes them suitable for applications where conventional humidity instruments may not provide sufficient sensitivity.
Continuous monitoring is another advantage. Operators can observe changing moisture conditions and identify unusual readings before they affect production or equipment performance.
These instruments also support preventive maintenance. Unexpected increases in moisture may indicate problems with gas dryers, filters, pipelines, or sampling systems. Early identification helps maintenance teams investigate the issue and reduce the risk of costly repairs.
Improved product quality is another important benefit. Industries that manufacture specialty gases, pharmaceuticals, and electronic components depend on controlled moisture levels to maintain consistent standards.
Digital connectivity in modern instruments also allows measurement results to be transferred to industrial control systems and data logging platforms. This supports better monitoring and documentation.
Factors to Consider When Selecting Trace Moisture Measurement Equipment
Choosing appropriate equipment requires careful evaluation of the application's measurement requirements. Different gases and industrial environments may require different sensing technologies and measurement ranges.
Measurement Sensitivity: The instrument should detect moisture concentrations within the required ppm or ppb range.
Accuracy: Reliable measurements are important when small changes in water vapor can affect product quality or process performance.
Gas Compatibility: Sensor materials and sampling components should be suitable for the gas being measured, particularly when working with reactive or corrosive gases.
Operating Pressure: Pressure conditions should be considered when selecting instruments and designing sampling arrangements.
Response Time: A suitable response time helps operators identify changes in moisture conditions efficiently.
Calibration Requirements: Regular calibration and accessible maintenance support help maintain long-term measurement reliability.
Businesses should also consider installation requirements, sampling line materials, and the availability of replacement sensors before purchasing equipment.
Importance of Sampling, Calibration, and Maintenance
Accurate moisture analysis depends not only on the instrument but also on the quality of the sampling system. Sampling lines should be selected carefully because certain materials can absorb or release moisture and influence measurement results.
Connections must be properly sealed to prevent atmospheric air from entering the system. Even small leaks can introduce unwanted moisture and produce misleading readings.
Calibration is equally important. Over time, sensors may experience performance changes because of aging, contamination, and operating conditions. Following the manufacturer's recommended calibration schedule helps maintain reliable measurements.
Regular inspection of filters, sampling lines, and connections can also prevent measurement problems. Technicians should review moisture trends and investigate unexpected changes to identify possible issues with drying equipment or gas handling systems.
How Dew-Point Supports Industrial Moisture Analysis
dew-point provides moisture measurement solutions designed to support industrial applications where accurate monitoring is essential. Reliable measurement technology helps businesses evaluate moisture conditions, monitor gas quality, and maintain suitable process environments.
When selecting appropriate equipment, industrial users should consider measurement sensitivity, accuracy, gas compatibility, operating pressure, and maintenance requirements. Choosing suitable instruments helps simplify moisture monitoring and supports better process management.
Consistent monitoring also helps businesses identify unwanted moisture, protect sensitive equipment, and maintain production quality. With appropriate measurement technology and proper calibration, industries can improve their moisture control procedures and reduce operational risks.
Conclusion
Accurate moisture monitoring is essential for industries that depend on dry gases and controlled environmental conditions. Even very small quantities of water vapor can affect equipment performance, gas purity, and manufacturing quality.
Specialized analyzers help detect low moisture concentrations and provide useful information for industrial process control. Selecting the right equipment requires evaluating measurement sensitivity, accuracy, gas compatibility, and calibration requirements.
By using reliable moisture measurement solutions and maintaining proper sampling arrangements, businesses can reduce moisture-related problems, protect valuable equipment, and achieve more consistent industrial performance.
0 comments
Log in to leave a comment.
Be the first to comment.