
The Importance of Trace Moisture Analysers in Industrial Applications
Moisture measurement plays a significant role in industries where maintaining controlled gas conditions is essential for product quality, equipment protection, and operational efficiency. Even very small amounts of water vapour can affect sensitive manufacturing processes, contribute to corrosion, and create difficulties in industrial equipment. Industries such as natural gas processing, petrochemicals, pharmaceuticals, power generation, and electronics require dependable monitoring solutions to maintain suitable moisture levels. Modern analytical instruments make it possible to detect low concentrations of water vapour and provide useful information about process conditions. By understanding the functionality and applications of moisture analysis equipment, businesses can select suitable technologies to improve production consistency and maintain reliable industrial operations.
Understanding the Purpose of Trace Moisture Analysers
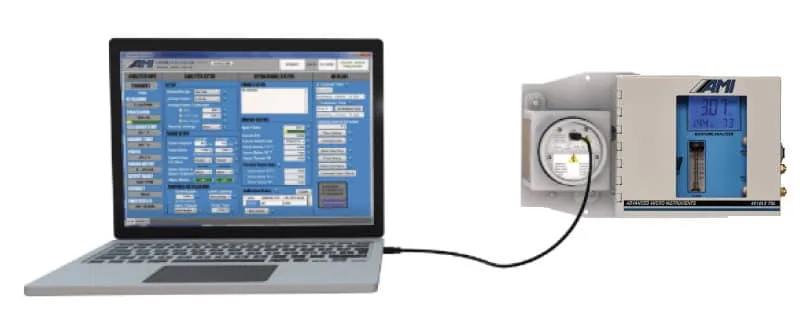
Trace moisture analyser equipment is designed to detect and measure extremely low concentrations of water vapour in gases and specialised industrial environments. These instruments are particularly useful when conventional humidity measurement devices cannot provide the required sensitivity. They help operators determine whether gas samples meet specific moisture requirements and whether industrial systems are operating within acceptable limits.
In many industrial applications, unwanted moisture can create serious challenges. It may contribute to pipeline corrosion, condensation, contamination, and reduced equipment performance. For example, natural gas processing facilities require effective moisture monitoring to maintain gas quality and protect transportation systems. Similarly, pharmaceutical and electronics manufacturers depend on controlled moisture conditions to protect sensitive materials.
Accurate measurements allow technical teams to identify moisture variations and take corrective action when necessary. This supports better process control and helps businesses maintain consistent production standards.
How Modern Moisture Analysis Technology Works
Moisture analysis instruments use different sensing technologies depending on the required measurement range and application. Each technology has specific operating principles and advantages.
Capacitive sensors detect changes in electrical capacitance caused by water vapour interacting with a sensing material. These sensors are commonly used in industrial monitoring systems because they can provide continuous measurements and support automated processes.
Chilled mirror technology works by cooling a reflective surface until water vapour begins to condense. The temperature at which condensation occurs represents the dew point. This approach is valued for its accuracy and is often used in applications requiring dependable reference measurements.
Aluminium oxide sensors are another option for detecting very low moisture concentrations. They measure changes in the electrical properties of a specialised sensing layer when exposed to water vapour. The resulting information can be converted into moisture readings.
Selecting the right technology depends on the gas composition, measurement range, operating pressure, temperature, and required accuracy.
Applications in Natural Gas and Petrochemical Industries
Natural gas processing facilities depend on accurate moisture measurement to maintain gas quality and protect pipelines. Excessive water vapour can cause condensation under certain pressure and temperature conditions. This may contribute to corrosion and create operational challenges throughout transportation and processing systems.
Petrochemical manufacturing also requires controlled moisture levels because water content can influence certain chemical reactions and production activities. Accurate monitoring helps operators maintain suitable process conditions and identify potential problems before they affect product quality.
Industrial gas manufacturers use analytical instruments to verify that their products meet specified moisture requirements. Consistent measurement supports quality assurance and helps maintain dependable gas supplies for different applications.
Importance in Pharmaceutical and Electronics Manufacturing
Pharmaceutical production involves materials that may be sensitive to environmental moisture. Some ingredients can absorb water from the surrounding atmosphere, potentially affecting their stability, quality, and storage conditions. Monitoring moisture levels helps manufacturers maintain controlled environments during processing, packaging, and storage.
The electronics industry also requires careful moisture management. Sensitive electronic components can be affected by excessive moisture during manufacturing and handling. In certain processes, unwanted water vapour may increase the risk of component damage or production defects.
Reliable moisture analysis provides manufacturers with useful information about environmental conditions. This supports quality control activities and helps businesses maintain consistent production standards.
Key Benefits of Advanced Moisture Analysis Instruments
One of the most important advantages of advanced analytical instruments is their ability to detect very low moisture concentrations. This is particularly valuable in industries where even minor variations can influence product quality or equipment reliability.
Another benefit is improved process control. Accurate readings allow operators to evaluate moisture conditions and make adjustments when required. This can reduce production interruptions and support more efficient industrial operations.
Modern instruments may also provide digital displays, automatic alarms, data logging, and communication capabilities, depending on the model. These features allow technicians to monitor measurement trends and maintain records for quality management.
Early moisture detection can also help protect industrial equipment. Identifying unwanted water vapour before it creates condensation or corrosion may reduce maintenance requirements and support longer equipment life.
Factors to Consider When Selecting an Analytical Instrument
Choosing suitable moisture analysis equipment requires careful evaluation of the intended application. Businesses should first identify the type of gas being measured and the expected moisture concentration. Different gases and operating environments may require specific sensor technologies.
Measurement range and accuracy are equally important. The selected instrument should be capable of detecting moisture levels relevant to the process. Operating temperature and pressure should also be considered because these conditions can influence measurement performance.
Other factors include response time, sensor lifespan, calibration requirements, installation arrangements, and maintenance support. Compatibility with existing industrial monitoring systems may also be useful for facilities that rely on automated process control.
A careful evaluation of these requirements helps businesses select equipment that meets their technical and operational needs.
Calibration and Maintenance for Reliable Performance
Regular calibration is essential for maintaining measurement accuracy. Over time, sensors may experience performance changes due to contamination, environmental exposure, or normal ageing. Calibration helps technicians identify deviations and verify that instruments continue to provide dependable readings.
Routine maintenance should include inspecting sampling lines, filters, sensor connections, and other system components. Contamination or leaks in the sampling arrangement may affect measurement results and reduce reliability.
Businesses should follow manufacturer recommendations for calibration intervals and maintenance procedures. Keeping proper service records also helps technical teams monitor instrument performance and plan preventive maintenance activities.
Supporting Industrial Efficiency Through Accurate Moisture Monitoring
Reliable moisture measurements provide valuable information for managing industrial processes. Operators can use measurement results to evaluate drying systems, identify unusual moisture changes, and maintain suitable operating conditions.
Monitoring also supports better energy management. Industrial drying equipment can consume considerable energy, so accurate readings help operators understand whether systems are working effectively. This may reduce unnecessary operation and improve resource utilisation.
Historical measurement data can further support process improvements. By reviewing previous readings, technical teams can identify recurring issues, evaluate equipment performance, and develop more effective maintenance strategies.
Conclusion
Moisture analysis is an important requirement in industries where even small amounts of water vapour can influence product quality, equipment performance, and process reliability. From natural gas processing and petrochemical manufacturing to pharmaceuticals and electronics, accurate monitoring helps businesses maintain suitable operating conditions. Selecting the right analytical instrument requires attention to sensing technology, measurement range, accuracy, operating environment, and calibration requirements. With appropriate equipment and regular maintenance, industries can improve process control, protect valuable assets, and maintain consistent production standards.
0 comments
Log in to leave a comment.
Be the first to comment.