
The Heat You Paid to Make Shouldn’t Be Getting a Free Ride
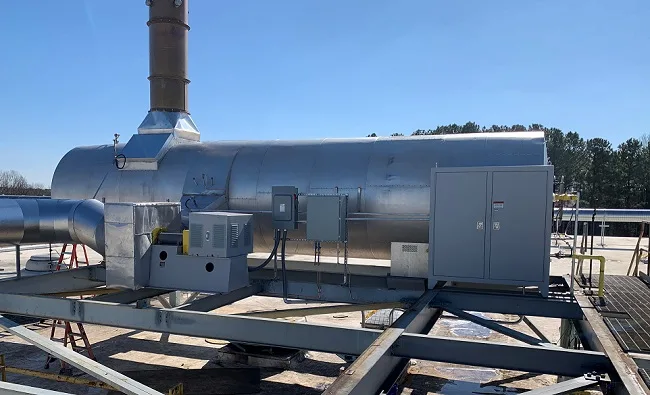
Your Process Is Making More Heat Than It Needs
Here is an awkward truth about industrial operations: generating heat is often necessary, but losing that heat usually is not.
Ovens, oxidizers, curing systems, cleaning processes, and other thermal equipment can produce significant amounts of hot exhaust. Once that heat leaves the process, it can disappear into the atmosphere carrying useful energy with it.
That is where modern heat recovery systems become interesting.
Instead of treating process heat as something that simply has to be exhausted, facilities can capture part of that energy and use it elsewhere. Depending on the application, recovered heat can support incoming air, water heating, combustion air, drying, preheating, or another compatible process.
The goal is not to make every thermal process complicated. It is to make the energy already being generated work a little harder.
The “Wait, We Already Heated That” Problem

Some industrial processes repeat the same energy-intensive cycle all day.
An industrial oven heats products. A paint booth handles coating operations. A thermal oxidizer treats process emissions. Thermal cleaning equipment removes contaminants from components.
Each application has its own requirements, but they can share one common challenge: hot exhaust streams leaving the process.
If that exhaust contains usable thermal energy, sending it directly outside can mean missing an opportunity for recovery.
Waste heat recovery systems are designed around this basic principle: capture useful heat before it disappears and transfer it to another part of the operation where it can provide value.
The exact configuration depends on temperature, airflow, contaminants, operating schedules, and the process itself. There is no universal recovery setup, which is precisely why proper process evaluation matters.
Heat Recovery Systems: Not a Magic Box

Heat recovery sounds simple until engineers start asking questions.
How hot is the exhaust?
How clean is it?
Is the temperature consistent?
What happens during startup and shutdown?
Can the recovered energy be used continuously?
What materials can tolerate the operating conditions?
Those questions determine whether a recovery approach makes technical and economic sense.
Heat recovery systems can use different methods and heat-exchanger arrangements depending on the application. Some transfer energy between exhaust and incoming process air. Others may support water or fluid heating.
The important point is that recovery should be designed around the process rather than forcing the process to fit a particular piece of equipment.
That distinction can make the difference between a useful energy strategy and an expensive piece of equipment sitting beside another expensive piece of equipment.
When an Industrial Oven Has More to Offer Than Heat
An industrial oven already has one obvious job: heating products or materials to a specified temperature.
But the exhaust leaving that oven may still contain substantial thermal energy.
Instead of allowing all of that energy to leave the building, a properly designed recovery arrangement can potentially preheat incoming air or support another compatible thermal demand.
This can reduce the amount of new energy required to reach operating temperatures.
The concept is especially relevant for processes that operate for long periods at relatively stable temperatures. Consistent operation generally makes it easier to identify where recovered heat can be used effectively.
Of course, oven design, exhaust characteristics, product requirements, and combustion configuration all matter. Recovery cannot interfere with temperature control, product quality, safety systems, or required ventilation.
Energy efficiency is useful. Predictable production is still the boss.
A Paint Booth Has Its Own Thermal Personality

Paint booth operations can involve ventilation, air movement, temperature control, and environmental requirements that make heat management particularly important.
A paint booth may require conditioned air to maintain suitable process conditions. At the same time, exhaust air can carry thermal energy away from the working area.
This creates an interesting engineering question: can energy from the outgoing stream be recovered without compromising airflow, contamination control, or coating quality?
In suitable applications, heat recovery can help precondition incoming air and reduce the energy required by heating or conditioning equipment.
But paint-related exhaust can also contain contaminants, so recovery equipment must be selected carefully. Heat exchangers and associated components need to be compatible with the exhaust characteristics and operating environment.
In other words, the hottest exhaust is not automatically the best candidate for recovery. Sometimes the dirtiest exhaust is the one that requires the most engineering attention.
Thermal Oxidizers: Hot by Design

A thermal oxidizer is designed to operate at elevated temperatures to treat certain process emissions.
That makes it an obvious candidate for discussions about heat recovery.
Once the treatment process has done its job, exhaust gases may still contain significant thermal energy. Depending on the system design, that energy can potentially be recovered to preheat incoming process air or combustion air.
This is one reason regenerative and recuperative approaches are commonly associated with thermal oxidizer applications.
The basic idea is straightforward: use thermal energy from the outgoing stream to reduce the amount of external energy needed to heat the incoming stream.
The engineering, however, is anything but casual.
Flow rates, temperature, contaminant loading, pressure drop, material selection, controls, and process variability all have to be considered. A recovery system must support emission-treatment requirements rather than create new operational problems.
The best thermal strategy is therefore not simply “recover as much heat as possible.” It is “recover useful heat while maintaining reliable process performance.”
Thermal Cleaning Equipment Has a Different Kind of Heat Story
Thermal cleaning processes use elevated temperatures to remove coatings, residues, polymers, oils, or other unwanted materials from components.
That makes thermal cleaning equipment inherently energy-intensive.
The challenge becomes particularly interesting when the process generates hot exhaust containing combustion products and removed material residues.
This is where thermal cleaning solutions can incorporate carefully engineered energy-management strategies.
Recovered heat may potentially support combustion air preheating or other compatible thermal requirements, depending on the process and exhaust composition.
However, thermal cleaning applications demand careful attention to contamination. The exhaust is not necessarily something you want casually circulating through another process.
Heat recovery therefore needs to consider not just temperature, but also what is actually present in the exhaust stream.
Hot air and clean air are not synonyms.
The Real Question: Where Can the Heat Go?
This is where energy discussions become more practical.
Capturing heat is only half the job.
The other half is finding a useful destination for it.
Imagine recovering a high-temperature exhaust stream from one process but having no nearby demand that can use the recovered energy. Technically, heat has been recovered. Practically, the system may not deliver much value.
Good waste heat recovery systems therefore begin with both sides of the equation:
Where is heat available?
and
Where is heat needed?
Potential applications can include combustion-air preheating, incoming-air preheating, water heating, drying processes, space heating, or other compatible operations.
The closer the temperature and timing of the heat source match the demand, the more interesting the opportunity becomes.
The Industrial Heat Compatibility Test
Think of this as a quick reality check before anyone starts drawing equipment diagrams.
Temperature: Is the available heat hot enough for the intended application?
Timing: Is the heat available when another process needs it?
Quality: Is the exhaust clean enough, or can indirect heat transfer be used safely?
Distance: Does the recovery opportunity require moving heat across half the facility?
Controls: Can the system respond to changing production conditions?
Maintenance: Can operators inspect and maintain the equipment without creating unnecessary downtime?
A technically possible recovery project may still be impractical if the recovered energy has nowhere useful to go.
Good engineering looks beyond the temperature number.
Interactive Break: Seven Questions Operators Actually Ask
Let’s make this less like a technical manual and more like the conversation that happens after someone notices the energy bill.
“Can Every Hot Exhaust Stream Be Recovered?”
Not necessarily. Temperature, contamination, airflow, process conditions, and available heat demand all matter.
“Are Waste Heat Recovery Systems Only Useful for Large Factories?”
No. The potential value depends on the quantity and quality of available heat, operating hours, energy costs, and how effectively the recovered energy can be used.
“Can Heat Recovery Affect Product Quality?”
It can if poorly designed. A properly engineered system should account for temperature stability, airflow, pressure drop, and process requirements.
“Can Recovery Work With a Thermal Oxidizer?”
Yes, thermal oxidizers are commonly considered in heat-recovery applications because their exhaust can contain substantial thermal energy. The specific recovery approach depends on the oxidizer design and process conditions.
“What Makes an Industrial Oven a Good Recovery Candidate?”
Long operating hours, consistent exhaust conditions, and a nearby demand for usable heat can make an oven worth evaluating.
“Is Hotter Always Better?”
Not automatically. A high-temperature stream can contain considerable energy, but contamination, materials compatibility, heat-transfer limitations, and the availability of a suitable heat sink all matter.
“Where Should We Start?”
Start with data rather than equipment.
Measure temperatures, airflow, operating hours, exhaust conditions, fuel consumption, and existing thermal demands. Those numbers can reveal where the strongest opportunities actually exist.
That is usually more productive than beginning with, “Which heat exchanger should we buy?”
Thermal Cleaning Solutions Need More Than a Temperature Gauge
Thermal cleaning solutions are often evaluated primarily around cleaning performance.
That makes sense. If the equipment cannot remove the required material reliably, energy efficiency will not rescue the process.
But modern thermal-system design increasingly looks at the entire operating cycle.
How much energy enters the system?
How much leaves with the exhaust?
How much can be recovered?
Where can that energy be reused?
How does recovery affect operating stability?
These questions connect cleaning performance with energy management.
For facilities running thermal cleaning equipment for extended periods, even incremental improvements can become meaningful when multiplied across operating hours.
The objective is not necessarily to redesign everything. Sometimes the opportunity is identifying one overlooked energy stream and giving it a useful destination.
The Future Is Less About Making More Heat
Industrial energy efficiency is gradually becoming less about simply asking equipment to consume less.
A more useful question is: What happens to the energy after the process uses it?
That shift changes the conversation.
A thermal oxidizer may become part of an energy-recovery strategy.
An industrial oven may become a source of preheating energy.
A paint booth may offer an opportunity to recover energy from conditioned exhaust.
Thermal cleaning equipment may provide another high-temperature stream worth evaluating.
None of these opportunities should be treated as automatic wins. Each requires engineering analysis, safety consideration, process compatibility, and economic evaluation.
But the principle is surprisingly simple.
If a process is already producing useful heat, there may be no good reason to let all of it leave the building unused.
The Practical Takeaway

The smartest heat-recovery project does not begin with a piece of equipment.
It begins with a map.
Map where heat enters the facility.
Map where heat leaves.
Map which processes need heat.
Then compare temperature, timing, flow, cleanliness, and operating conditions.
That exercise can reveal connections that are easy to miss when every thermal process is viewed independently.
Heat recovery systems, thermal cleaning equipment, paint booths, industrial ovens, and thermal oxidizers may look like completely different parts of an industrial operation.
From an energy perspective, however, they can all be pieces of the same conversation.
The heat is already there.
The interesting question is whether the process gets to use it twice.
0 comments
Log in to leave a comment.
Be the first to comment.