
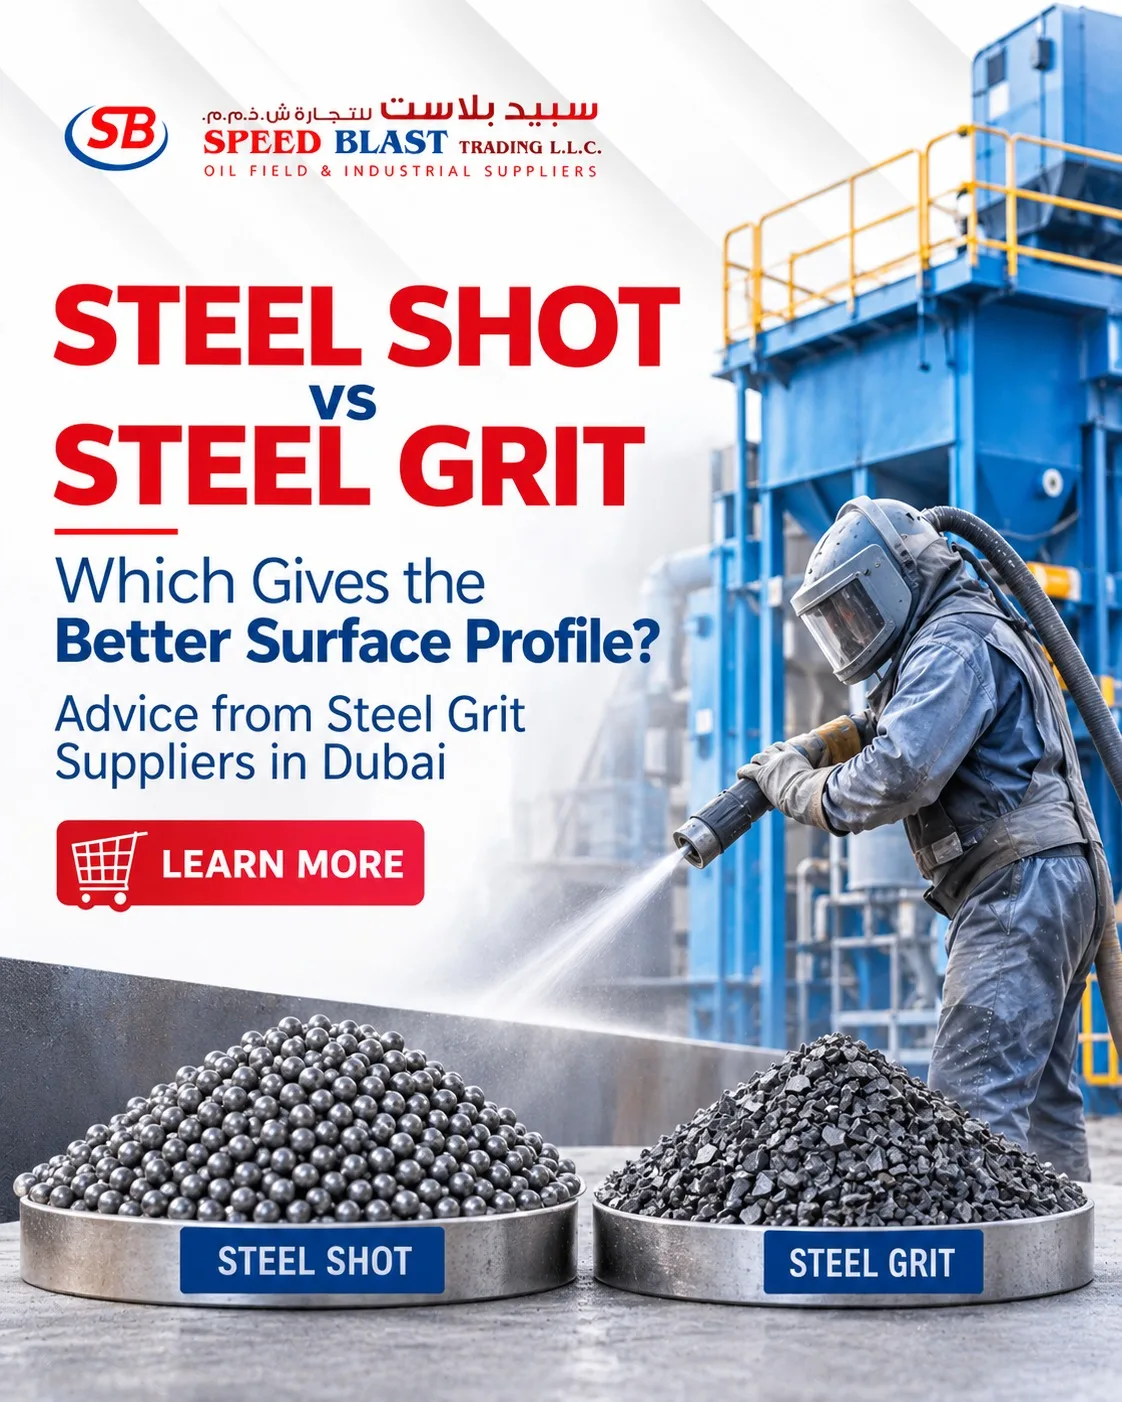
Steel Shot vs Steel Grit: Which Gives the Better Surface Profile? Advice From Steel Grit Suppliers in Dubai
Speed Blast Trading LLC
A coating can fail within months even when the paint is excellent. The cause is often the surface underneath: the wrong profile, left by the wrong abrasive.
If you are weighing up steel grit suppliers in Dubai, it helps to know what shot and grit each do to steel before you place an order. This guide explains how they differ, what each does to the surface, and how to match the abrasive to the job.
What “Surface Profile” Actually Means
Surface profile is the microscopic pattern of peaks and valleys that blasting leaves on steel. It is the anchor pattern your primer grips.
Two things matter: the depth of the profile and its shape. Too shallow, and the coating has little to hold onto. Too deep, and the peaks can poke through a thin paint film, which is a common starting point for early rust spots.
The coating manufacturer’s data sheet states the profile range the system needs. That document, not the abrasive, should lead the decision.
How Steel Shot Works
Steel shot is made of round, spherical particles. When it hits the surface, it hammers rather than cuts.
That has a few practical effects:
It peens the steel, leaving a rounded, dimpled texture.
It cleans scale and light contamination without gouging the metal.
It tends to give a more uniform, shallower profile.
Shot is usually chosen for cleaning, for peening, and where a smoother anchor pattern is wanted. Its weakness is that it is not efficient at cutting through heavy rust or thick, hard mill scale. On its own, it can leave a surface that looks clean but has a profile too rounded for some high-performance coatings.
How Steel Grit Works
Steel grit is angular and sharp-edged. It cuts into the surface rather than pounding it.
The result is a rougher, sharper, more jagged profile with distinct peaks. For most protective coatings, that is what you want, because the paint locks into the surface mechanically.
Grit also removes heavy rust and mill scale faster. The trade-off is that it wears machine parts more quickly, and a very coarse grit on thin plate can leave a profile deeper than the coating needs.
Steel Shot vs Steel Grit: The Practical Comparison
Here is how the two compare in everyday use.
Profile shape. Shot gives a rounded, peened pattern. Grit gives a sharp, angular one.
Cleaning speed on heavy scale. Grit is generally faster. Shot is gentler.
Coating adhesion. Grit’s angular profile suits most industrial coatings. Shot’s smoother profile suits some systems and specific requirements.
Wear on equipment. Shot is kinder to nozzles and wheels. Grit is harder on them.
Abrasive life. Round shot tends to last longer through repeated use, while grit breaks down into smaller fragments faster. This varies with the job and the machine.
Neither is better in every case. Each suits a different job.
The Case for a Working Mix
Many operations use neither on its own. Blending shot and grit gives some of the cutting power of grit with some of the peening action of shot, and can produce a profile that suits a wide range of coating specifications.
The right ratio depends on the steel, the starting condition and the coating system. Start from the specification and adjust from there, rather than guessing.
Matching the Abrasive to Shot Blasting Machines in UAE
The abrasive you choose has to suit your equipment. This is where many buyers run into trouble.
When selecting shot blasting machines in UAE, check what the machine is built to handle. Steel abrasives are heavy and hard, so they need suitable hoses, nozzles and valves, and they wear worn parts fast. A machine set up for lighter, expendable abrasives may not tolerate steel well.
Blast pots in 20L, 50L, 100L and 200L sizes are common choices, and the pot size affects how long you can blast before refilling. Nozzle condition matters too. A worn nozzle changes both the air flow and the profile you get.
Matching the Abrasive to the Job
Here is a simple way to think about it.
Heavy Rust and Thick Mill Scale
Grit, or a grit-heavy mix, cuts faster and reaches bare metal sooner. This is typical on structural steel and older plate.
New Steel Needing Light Cleaning
Shot, or a mix with more shot, can clean without over-roughening the surface.
High-Performance Protective Coatings
Check the data sheet for the required profile. Most call for an angular profile, which points toward grit or a blend.
Pipe and Tank Work
Internal surfaces may need specialist tools. Hollo Blast and Spin Blast systems are designed for internal pipe blasting, so abrasive choice should be confirmed against the tool.
Local Conditions That Affect Your Result
Dubai’s heat and humidity change how quickly a blasted surface starts to flash rust. Freshly blasted steel can discolour within hours in humid conditions, so coating soon after blasting matters.
Coastal work adds another risk: salt contamination. Chlorides trapped in the surface can cause blistering under the paint, even when the profile is perfect. A clean, dry abrasive helps, and so does testing the surface before coating.
Oil and gas, marine and shipyard work often come with strict surface preparation requirements, so confirm the specification before you buy.
Common Mistakes to Avoid
Choosing the abrasive by habit rather than by the coating specification.
Reusing abrasive that is contaminated with oil, salt or moisture.
Skipping profile checks because the surface “looks right.”
Running worn nozzles that change the blast pattern.
Blasting more than you can coat before flash rust appears.
How to Check Your Profile
Do not rely on appearance. Replica tape such as Testex tape lets you measure the profile height after blasting. A Bresle patch tests for soluble salts, which is especially important near the coast. Blotting paper checks compressed air for oil and moisture contamination, which can ruin an otherwise good surface.
Check at the start of the job, and again whenever the abrasive, nozzle or air supply changes.
Buying Steel Abrasives: What to Ask
Before you order, ask your supplier:
Which grade or size suits your coating specification?
Is a shot, grit or blended mix the better fit for your machine?
What accessories or spare parts will you need for steel abrasives?
A good supplier will ask about your equipment and coating system before recommending anything.
Frequently Asked Questions
Which Gives a Better Surface Profile, Steel Shot or Steel Grit?
Neither is better in every case. Grit gives a sharper, deeper anchor profile that suits most coatings, while shot gives a rounder, shallower one. Always follow the coating data sheet.
Can I Use Steel Shot and Steel Grit Together?
Yes. A blended working mix is common and can balance cleaning speed with profile shape. The right ratio depends on the steel and the coating system.
Is Steel Shot Blasting in Dubai Affected by Humidity?
Yes. Humid conditions speed up flash rust on freshly blasted steel, so coat promptly and keep abrasives and air supply dry.
Do Steel Abrasives Wear Out Blasting Equipment Faster?
They can, especially grit. Check nozzles, valves and hoses regularly, and replace worn parts before they affect the blast pattern.
What Should I Look for in Shot Blasting Machines in UAE?
Look for a machine suited to steel abrasives, with the right pot size, durable accessories and reliable air treatment. Moisture separators and after coolers help keep the abrasive dry.
Talk to Speed Blast Trading LLC
Speed Blast Trading LLC has supplied blasting, painting and coating equipment, abrasives and safety products since 2009. We stock garnet, steel shot, steel grit, copper slag and aluminium oxide, alongside blasting machines, accessories, inspection tools and PPE. We also offer equipment rental and repair for sandblasting machines and painting pumps.
If you need steel shot blasting in Dubai, tell us about your steel, your coating system and your equipment, and we will help you choose the right abrasive and the right accessories.
Our head office is in Dubai Investment Park 2 (DIP 2), Dubai, and we have a branch in Mussafah, Abu Dhabi.
Phone and WhatsApp: +971 55 363 8835
Email: [email protected]
Working hours: 9 to 5
0 comments
Log in to leave a comment.
Be the first to comment.