
Rubber Belt Conveyor: Durable Material Handling for Industrial Operations
Industrial facilities often need to transport heavy materials, packaged products, and bulk goods across different processing areas. Choosing the right conveyor system can improve material flow and support consistent operations. A rubber belt conveyor is a widely used material handling solution because its durable belt surface can provide reliable transportation in demanding working environments. With suitable construction and maintenance, it can serve industries that handle a variety of materials every day.
What Is a Rubber Belt Conveyor?
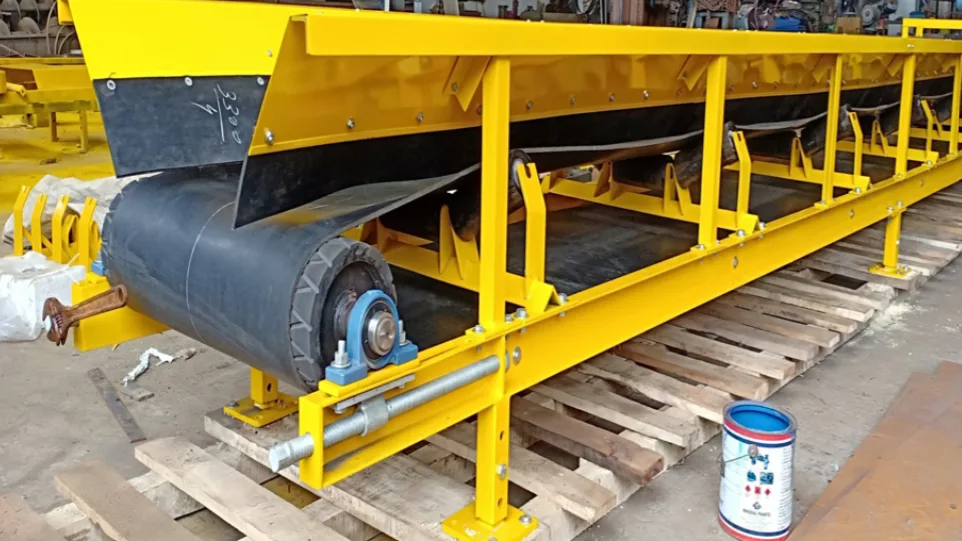
A rubber belt conveyor is a mechanical system that moves materials along a continuous rubber belt supported by rollers or a conveyor bed. The belt travels around drive and return pulleys, while a motor powers the movement in most industrial applications.
Rubber belts are available in different thicknesses, strengths, and surface designs. Some are reinforced with fabric or steel cords to improve tensile strength and resistance to demanding loads. The appropriate belt construction depends on the material being carried, operating conditions, and required service life.
How Does a Rubber Belt Conveyor Work?
The conveyor motor rotates the drive pulley, moving the belt along its designated route. Materials are loaded onto the belt at one point and transported toward a discharge location. Supporting rollers help maintain the belt's path and carry the load throughout the conveying process.
For inclined applications, specially designed belt surfaces or cleats can help prevent materials from slipping. Belt tension, pulley alignment, and loading conditions must be correctly managed to maintain smooth operation.
The conveyor can be designed for horizontal transportation, inclined movement, or customized layouts according to the facility's requirements.
Applications Across Different Industries
A rubber belt conveyor is used in mining, cement production, construction, agriculture, recycling, manufacturing, and material processing. Mining facilities may use heavy-duty belts to transport suitable minerals and extracted materials. Cement plants can use conveyor systems to move raw materials between storage and processing areas.
Agricultural operations may use them for handling grains and other bulk products, while recycling facilities can transport selected waste materials through sorting and processing stages. Manufacturing plants may also use rubber belt conveyors for moving industrial components and finished goods.
The belt grade and conveyor configuration should always match the material's weight, temperature, abrasiveness, and environmental conditions.
Major Advantages of Rubber Belt Conveyors
One important advantage is durability. Properly selected rubber compounds can provide resistance to abrasion, impact, and demanding operating conditions. Reinforced belt constructions can also support heavier loads when designed for the application.
Another benefit is continuous transportation. A rubber belt conveyor can move materials over considerable distances, helping connect separate work areas and reducing repeated manual handling.
Different belt specifications are available for specific requirements, including heat resistance, oil resistance, and abrasion resistance. This allows businesses to choose a belt suited to their working environment instead of relying on a single design for every application.
When integrated into a well-planned material handling system, rubber belt conveyors can support organized operations and consistent material flow.
How to Choose the Right Rubber Belt Conveyor
Before purchasing a rubber belt conveyor, evaluate the material type, load weight, particle size, and required conveying capacity. Consider conveyor length, belt width, operating speed, incline, and the layout of the facility.
Environmental conditions are equally important. High temperatures, moisture, oils, sharp materials, and abrasive surfaces can affect belt performance. Selecting the correct rubber compound and reinforcement can help improve reliability.
Businesses should also assess motor capacity, frame strength, installation requirements, and compatibility with existing equipment. Professional guidance can help determine the appropriate specifications.
Maintenance and Safety
Regular maintenance helps extend conveyor life. Inspect the belt for cracks, cuts, edge damage, and excessive wear. Check rollers, pulleys, bearings, belt tracking, and tension according to the manufacturer's recommendations.
Remove material buildup and address unusual vibration or belt slippage promptly. Safety guards and emergency stops should remain functional, and workers must follow proper isolation procedures before maintenance.
Conclusion
A rubber belt conveyor provides a dependable option for transporting materials across many industrial environments. Its durable construction, range of belt specifications, and ability to support continuous movement make it valuable for demanding applications. Selecting the right design and following regular maintenance practices can help businesses improve material handling efficiency and achieve reliable long-term performance.
0 comments
Log in to leave a comment.
Be the first to comment.