
Pressure Relief Valve: How It Protects Industrial Systems From Excessive Pressure
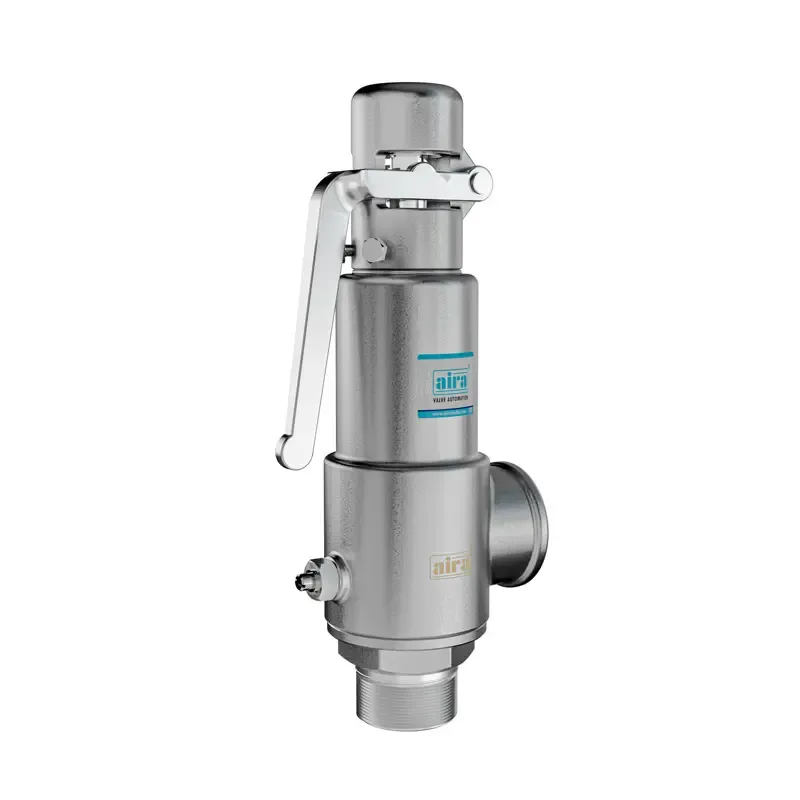
Maintaining safe pressure levels is essential for reliable industrial operations. Many systems handle liquids, gases, steam, or other fluids under pressure, and excessive pressure can damage equipment, disrupt production, and create serious safety risks. A pressure relief valve helps protect these systems by releasing excess pressure when it reaches a predetermined limit. Choosing a suitable Pressure Relief Valve Manufacturer is an important step toward ensuring that the valve meets the application's pressure, temperature, and safety requirements.
What Is a Pressure Relief Valve?
A pressure relief valve is a safety device designed to open when system pressure reaches a specified set pressure. It releases excess fluid to help prevent pressure from exceeding acceptable limits. Once the pressure decreases, the valve may close again, depending on its design and operating characteristics.
These valves are used in pressure vessels, boilers, pipelines, compressors, pumps, storage tanks, and various industrial processing systems. Their primary purpose is to provide overpressure protection for equipment and connected components.
A pressure relief valve should not be confused with a pressure reducing valve. A pressure reducing valve controls downstream operating pressure, while a pressure relief valve protects a system by releasing excess pressure.
How Does a Pressure Relief Valve Work?
Most conventional pressure relief valves operate through a mechanism that responds to system pressure. In a spring-loaded design, the spring applies a closing force to keep the valve shut during normal operation.
When the system pressure reaches the specified set pressure, the force exerted by the fluid overcomes the closing force, allowing the valve to open. Excess fluid is then discharged through the designated outlet or relief system.
As pressure falls, the closing mechanism returns the valve toward its seat. The exact opening, closing, and reseating behaviour depends on the valve design and the application.
Correct sizing and installation are essential. A valve that is incorrectly selected may not provide the required protection under actual operating conditions.
Why Pressure Relief Valves Are Important
Excessive pressure can result from blocked outlets, thermal expansion, equipment malfunction, chemical reactions, or unexpected changes in operating conditions. Without suitable protection, pressure may exceed the limits of the equipment.
Pressure relief valves help manage these risks by providing a designed path for excess pressure to escape. They can protect pipelines, vessels, and other pressure-containing components from potentially dangerous operating conditions.
Their effectiveness depends on correct selection, proper installation, regular inspection, and compliance with relevant safety standards. A relief valve is one part of an overall protection strategy and does not replace other necessary safety controls.
Important Factors When Selecting a Pressure Relief Valve
Choosing the correct valve requires a detailed understanding of the system. Consider the following factors before making a selection:
• Set pressure: Select a valve with a set pressure appropriate for the protected equipment and applicable design requirements.• Flow capacity: Ensure the valve can discharge the required amount of fluid during the specified overpressure scenario.
• Fluid compatibility: Verify that the body, seat, seals, and internal components are suitable for the process fluid.
• Operating temperature: Confirm that the valve materials can withstand the expected temperature range.
• Connection and installation: Check connection sizes, outlet arrangements, flow direction, and available installation space.
• Applicable standards: Review relevant industry codes, certifications, and inspection requirements for the application.
These factors help ensure that the valve can perform its intended safety function reliably.
Industrial Applications of Pressure Relief Valves
Pressure relief valves are widely used in oil and gas facilities, chemical processing plants, steam systems, power generation equipment, water treatment installations, compressed-air systems, and manufacturing facilities.
In boilers and steam equipment, they help protect pressure-containing components from excessive pressure. In chemical processing, appropriately specified relief valves can protect vessels and pipelines during abnormal operating conditions. In compressed-air systems, they help prevent pressure from exceeding the permitted limits of protected equipment.
Mark & Aira Trading LLC is a name businesses may consider when exploring industrial valve supply options. Before purchasing, buyers should verify the valve's technical specifications, suitability for the intended application, and compliance with relevant safety requirements.
Maintenance and Inspection
Regular inspection is essential for maintaining pressure relief valve performance. Depending on the application, maintenance may include checking for corrosion, leakage, blockage, damaged components, and signs of improper operation.
Testing and servicing should follow the manufacturer's instructions and applicable regulations. Never adjust a valve's set pressure without proper authorization and suitable testing procedures. Before maintenance, the system must be isolated and made safe by qualified personnel.
Conclusion
Pressure relief valves play a vital role in protecting industrial systems from excessive pressure. By selecting the correct set pressure, discharge capacity, materials, and valve design, businesses can improve equipment protection and operational reliability. Proper installation, inspection, and maintenance are equally important for ensuring that the valve performs its intended safety function when required.
0 comments
Log in to leave a comment.
Be the first to comment.