
Industrial Valves in Modern Manufacturing: Engineering, Quality and Performance
Modern manufacturing industries depend on efficient fluid control systems to maintain productivity, operational safety, and consistent product quality. From chemical processing and pharmaceuticals to oil and gas, water treatment, and power generation, industrial valves play a critical role in regulating the movement of liquids, gases, steam, and other process media.
With increasing industrial automation and technological advancements, the demand for reliable valve solutions continues to grow. Every industrial application has specific operating requirements, making engineering precision, material selection, and manufacturing quality essential considerations. An experienced industrial valves manufacturer focuses on developing solutions that deliver dependable performance under different operating conditions.
1. Importance of Industrial Valves in Manufacturing
Industrial valves are essential components of pipeline and process control systems. They help regulate, isolate, direct, and prevent the unwanted movement of fluids throughout industrial facilities.
Proper valve selection allows manufacturing plants to maintain stable operating conditions while reducing unnecessary pressure losses, leakage risks, and equipment downtime.
Industrial valves are commonly used in:
• Oil and gas processing facilities.• Pharmaceutical and biotechnology plants.
• Chemical and petrochemical industries.
• Food and beverage manufacturing.
• Water treatment and distribution systems.
• Power generation and energy facilities.
Each application requires valves designed according to its operating pressure, temperature, flow rate, and media characteristics.
2. Engineering and Design Considerations
Engineering plays an important role in determining the performance and reliability of industrial valves. Manufacturers must consider several technical factors before developing a valve for a particular application.
Valve design involves selecting suitable dimensions, pressure ratings, connection types, sealing arrangements, and operating mechanisms.
Modern engineering technologies, including computer-aided design (CAD) and precision machining, help improve dimensional accuracy and product consistency.
Important design considerations include:
• Operating pressure and temperature requirements.• Flow characteristics and fluid compatibility.
• Valve size and pipeline connection standards.
• Sealing performance and leakage prevention.
• Maintenance accessibility and operating life.
Careful engineering helps ensure that valves perform effectively throughout their intended service conditions.
3. Material Selection for Better Performance
Material selection directly influences the durability, corrosion resistance, and overall performance of industrial valves.
Different industries handle different types of fluids, including corrosive chemicals, high-temperature steam, compressed air, and hygienic process media. Therefore, selecting the correct construction material is essential.
Commonly used materials include:
• Stainless Steel: Offers corrosion resistance and is widely used in hygienic and chemical applications.• Carbon Steel: Suitable for many high-pressure industrial environments.
• Cast Iron: Commonly used in general industrial and water-handling systems.
• PVC and UPVC: Used in selected chemical and water distribution applications.
• CPVC and PPH: Suitable for specific applications involving chemical exposure and demanding operating conditions.
The correct material should always be selected according to the process requirements and applicable engineering standards.
4. Quality Control and Manufacturing Standards
Quality assurance is a fundamental part of industrial valve manufacturing. A properly manufactured valve must meet its specified operating requirements and maintain dependable performance during service.
Manufacturing facilities use different inspection and testing procedures to verify product quality.
These include pressure testing, leakage testing, dimensional inspection, material verification, and functional testing.
Relevant international standards, such as API, ASME, ANSI, and ISO, provide important guidelines for valve design, manufacturing, inspection, and performance, depending on the product category.
Consistent quality control helps reduce operational risks and improves equipment reliability.
5. Automation and Technological Advancements
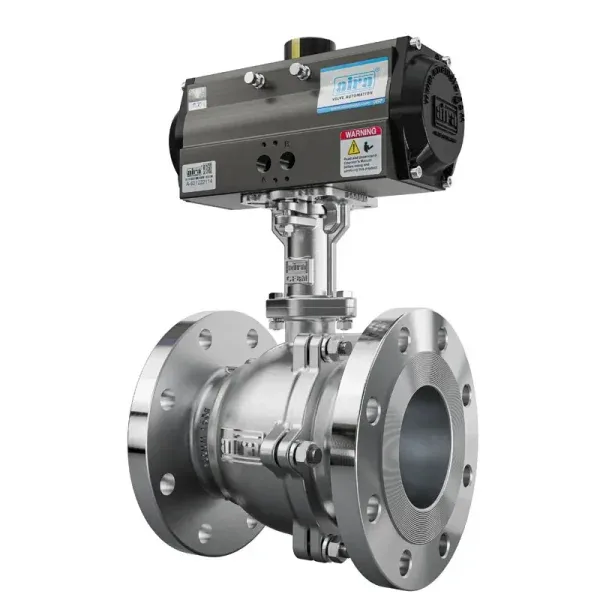
Industrial automation is changing the way valves operate within modern manufacturing facilities. Pneumatic and electric actuators allow valves to be controlled automatically, reducing the need for continuous manual operation.
Automated valve solutions can improve process accuracy and support integration with industrial control systems.
Some important technological developments include:
• Pneumatic and electric actuator integration.• Smart valve monitoring systems.
• Advanced sealing technologies.
• Automated inspection and testing equipment.
• Digital process monitoring and predictive maintenance.
These innovations are helping industries improve operational efficiency and maintain better control over manufacturing processes.
Aira Euro Automation Pvt Ltd is associated with the industrial valve and automation sector, where engineering quality and reliable flow control solutions are important considerations.
6. Future of Industrial Valve Manufacturing
The future of industrial valve manufacturing will be influenced by advanced materials, automation, sustainable production methods, and smart monitoring technologies.
Manufacturers are increasingly focusing on developing durable products that reduce maintenance requirements, improve energy efficiency, and support changing industrial applications.
As industries continue to modernize, the importance of precision engineering, reliable sealing, and application-specific valve solutions will become even greater.
Conclusion
Industrial valves remain essential components of modern manufacturing infrastructure. Their performance directly influences process efficiency, operational safety, and equipment reliability.
By prioritizing engineering precision, appropriate material selection, strict quality control, and technological innovation, the industrial valve sector can continue supporting the evolving requirements of manufacturing industries worldwide.
0 comments
Log in to leave a comment.
Be the first to comment.