
Industrial Heat Has a Second Shift. Is Anyone Putting It to Work?
For facility managers and process engineers, this raises a practical question: could the heat already being generated help reduce energy demand elsewhere?
Waste Heat Recovery Systems: Making the Numbers Work Harder

Heat leaving an industrial process is not necessarily energy that has lost its value. With the right equipment and application, some of it can be recovered and reused.
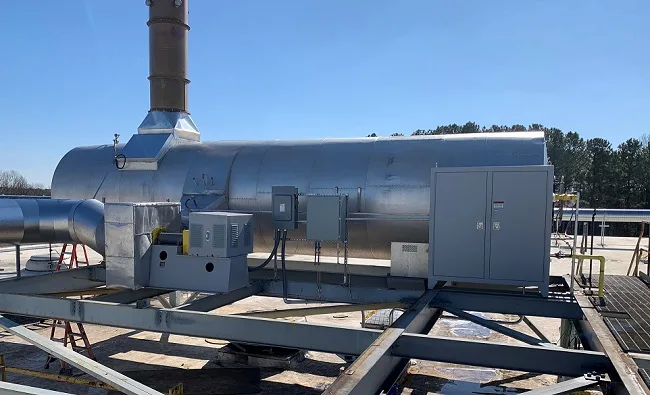
Waste heat recovery systems capture thermal energy from exhaust gases or other hot streams and transfer it to another suitable process. Depending on the facility, that energy might preheat combustion air, warm incoming process air, or support water-heating and drying operations.
However, recovering heat is not automatically a profitable investment. Engineers must evaluate installation costs, maintenance requirements, production schedules, and expected energy savings before recommending a system.
Industrial Ovens: Where Exhaust Deserves a Closer Look

An industrial oven needs reliable temperature control to deliver consistent results. Yet the exhaust leaving the system may still contain energy that could serve another purpose.
In suitable applications, heat recovery systems can transfer energy from outgoing exhaust to incoming air, reducing the additional energy required to reach operating temperatures.
For manufacturers running ovens for long production cycles, this opportunity can be worth investigating. Longer operating hours may provide more opportunities to use recovered heat, particularly when temperatures and exhaust flows remain reasonably consistent.
The design must still protect product quality, ventilation, and process stability. A recovery system should support the oven's performance rather than introduce unnecessary complexity.
Paint Booths: Efficiency Without Compromising Finish Quality
The functioning of a paint booth takes a specific airflow, proper ventilation and an ideal atmosphere. If a function of a paint booth is maintained, it could account for the energy needs of the facility.Based on exhaust properties and safety conditions, heat recovery may be used to partially preheat the incoming air using heat from an exhaust stream. This can lower heating loads and maintain coating process requirements.Critical shortcoming: paint fumes potentially include volatile substances and other impurities. Every recovery setup will need to factor in these substances, fire hazards, and any relevant requirements for the ventilation of fumes.What's the first consideration for B2B decision-makers? Energy performance can be the most important consideration—at least until the coated product is delivered and the operation doesn't perform as expected.
Thermal Oxidizers: Recovering Energy After Emissions Treatment

How treatment should be carried out will depend upon the composition of the exhaust, its temperature and flow rate, on what is required in treatment and on what recovered heat is to be used.Keeping control of emissions remains a key focus. Recovery plant must be integrated with the oxidiser control and safety systems, an engineered design based on a risk assessment.
Thermal Cleaning Equipment: Beyond the Cleaning Cycle
Thermal cleaning equipment removes coatings, residues, and other The functioning of a Thermal cleaning equipment takes a specific airflow, proper ventilation and an ideal atmosphere. If a function of a paint booth is maintained, it could account for the energy needs of the facility.Based on exhaust properties and safety conditions, heat recovery may be used to partially preheat the incoming air using heat from an exhaust stream. This can lower heating loads and maintain coating process requirements.Critical shortcoming: paint fumes potentially include volatile substances and other impurities. Every recovery setup will need to factor in these substances, fire hazards, and any relevant requirements for the ventilation of fumes.What's the first consideration for B2B decision-makers? Energy performance can be the most important consideration—at least until the coated product is delivered and the operation doesn't perform as expected.
The most suitable solution balances cleaning effectiveness, energy consumption, environmental requirements, and long-term operating reliability.
The Engineering Reality Check: Five Questions Before Investing

Before approving a recovery project, decision-makers need more than an attractive estimate of potential savings.
1. Is enough heat available?
Measure exhaust temperatures and flow rates to establish how much usable thermal energy the process provides.
Questions From Plant Managers
Can every facility benefit from heat recovery systems?
No. The opportunity depends on available heat, operating schedules, energy costs, and whether recovered energy can be used effectively.
A Better Return on Energy Starts With Better Planning

For industrial businesses, energy efficiency is most valuable when it supports measurable operational and financial goals.
An industrial oven, paint booth, thermal oxidizer, and thermal cleaning equipment serve different purposes, but each may present opportunities to examine how energy is used and where it goes.
Well-designed heat recovery systems can help facilities reduce avoidable energy demand without compromising product quality, process reliability, or safety.
0 comments
Log in to leave a comment.
Be the first to comment.