
How Proper Coolant Use Improves Cutting Tool Performance and Tool Life
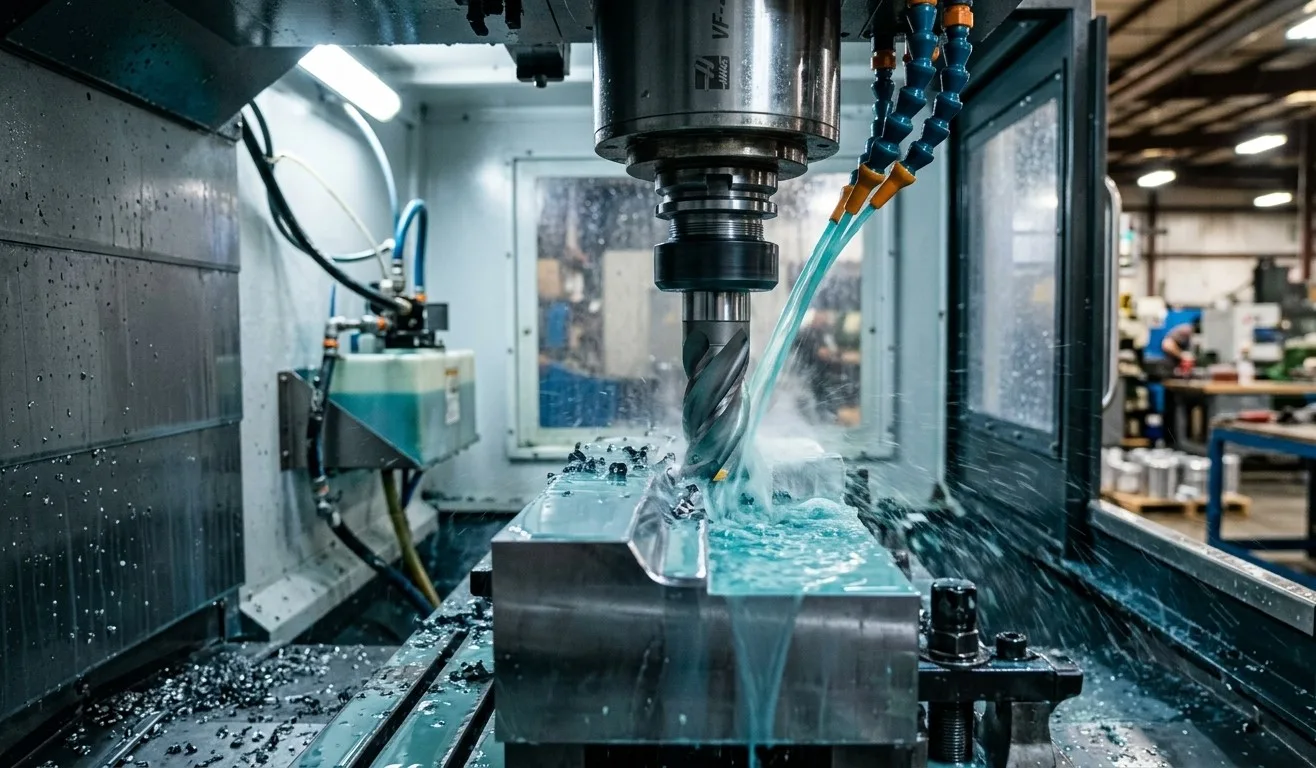
In modern manufacturing and machining, cutting tools operate under demanding conditions involving friction, heat, pressure, and continuous material removal. Without proper thermal and lubrication control, even high-quality tools can experience premature wear, poor surface finish, dimensional inaccuracies, and unexpected failure. Proper coolant use is therefore an important part of maintaining consistent machining performance and extending tool life.
For manufacturers and engineering workshops, selecting suitable tooling is only one part of the process. Using the right coolant, applying it correctly, and maintaining the coolant system can significantly influence the performance of industrial cutting tools. Khokhawala Trading LLC, an experienced Industrial Tools Supplier in Dubai, provides industrial tooling solutions for machining, manufacturing, maintenance, and engineering applications.
What Is Machining Coolant?
Machining coolant is a fluid used during cutting operations to help control heat, reduce friction, improve chip evacuation, and protect both the cutting tool and workpiece.
Depending on the machining process, coolant may be applied as a continuous stream, mist, high-pressure jet, minimum quantity lubrication (MQL), or other controlled delivery method.
Common types include:
- Water-soluble cutting fluids
- Semi-synthetic coolants
- Synthetic coolants
- Straight cutting oils
- Specialized lubricating fluids
The correct coolant depends on the workpiece material, cutting tool, machining operation, machine configuration, and required production conditions.
Why Coolant Is Important for Cutting Tools
During machining, the cutting edge experiences significant friction and heat. Cutting speeds and feeds can generate temperatures high enough to accelerate tool wear and affect the workpiece.
Proper coolant application can help manage these conditions in several ways.
1. Controls Cutting Temperature
Heat is one of the primary causes of cutting tool wear. Excessive temperature can soften certain tool materials, accelerate coating degradation, and promote thermal cracking.
Coolant absorbs and carries away heat from the cutting zone, helping maintain more stable operating conditions.
Temperature control becomes especially important during high-speed machining, deep cuts, and operations involving difficult-to-machine materials.
2. Reduces Friction
Coolants can provide lubrication between the cutting tool, workpiece, and chips. Reduced friction can lower cutting forces and decrease heat generated at the interface.
Lower friction can help the cutting edge maintain its condition for longer, particularly when machining materials that tend to generate high friction or adhere to the tool.
3. Improves Chip Evacuation
Efficient chip removal is essential in CNC machining. If chips remain trapped around the cutting zone, they can recut against the workpiece or cutting tool.
A properly directed coolant stream can help move chips away from the cutting area. This is particularly useful in drilling, deep pocketing, grooving, and other operations where chip evacuation can be challenging.
4. Protects Surface Finish
Stable thermal conditions and effective chip evacuation can contribute to better surface finish.
When chips are repeatedly recut or heat builds up in the machining zone, the finished surface may develop scratches, discoloration, built-up material, or other defects.
Proper coolant delivery helps create more consistent cutting conditions.
How Coolant Affects Tool Life
Tool life refers to the usable operating period of a cutting tool before wear reaches an unacceptable level or the tool can no longer maintain the required machining performance.
Coolant can influence several common wear mechanisms.
Flank Wear
Flank wear occurs along the clearance face of the cutting tool. Excessive heat and friction can accelerate this form of wear.
Effective cooling and lubrication can help slow the progression of flank wear under suitable machining conditions.
Crater Wear
Crater wear develops on the rake face of a cutting tool because of contact with hot chips. High temperatures and chemical interaction between the chip and tool material can contribute to crater formation.
Proper coolant selection and application may help manage heat and reduce the severity of certain wear conditions.
Thermal Cracking
Rapid temperature changes can cause thermal stress in some cutting tools. Intermittent cutting operations, such as milling, can expose cutting edges to repeated heating and cooling cycles.
In certain applications, uncontrolled coolant delivery can contribute to thermal shock. Therefore, coolant should not automatically be considered beneficial in every cutting operation. The tool manufacturer's recommendations and the specific machining process should determine whether continuous coolant, intermittent coolant, or dry machining is appropriate.
Selecting the Right Coolant for the Application
Not every coolant is suitable for every machining operation. The choice should consider several factors.
Workpiece Material
Different materials respond differently to coolant and lubrication.
For example:
- Aluminum may require fluids that reduce material adhesion.
- Stainless steel may benefit from effective lubrication and heat control.
- Cast iron is often machined dry or with controlled coolant depending on the application.
- Hardened materials may require specialized machining strategies.
- Non-ferrous alloys can have specific requirements related to staining or chemical compatibility.
The coolant should be compatible with both the material and the machining process.
Cutting Tool Material
Tool material also affects coolant selection. Carbide cutting tools, high-speed steel tools, ceramic tools, and other tool materials have different thermal characteristics.
For coated carbide tooling, coolant compatibility can also be important for protecting the coating and maintaining predictable performance.
Machining Operation
Turning, milling, drilling, threading, grooving, and reaming can have different coolant requirements.
For example, drilling often benefits significantly from effective coolant delivery because chips must travel through a confined hole. Deep-hole applications may require specialized high-pressure coolant systems.
Proper Coolant Delivery Matters
Using the correct coolant is not enough. It must reach the cutting zone effectively.
Direct the Coolant at the Cutting Edge
The coolant stream should be positioned so that it reaches the area where heat and friction are generated.
Poorly positioned nozzles may spray coolant onto the workpiece or tool holder without adequately reaching the cutting edge.
Use Appropriate Flow and Pressure
Flow rate and pressure should match the machining operation and machine system.
High-pressure coolant can be useful for demanding applications, particularly where chip evacuation is difficult. However, excessive pressure or unsuitable application can create other problems.
Always follow the recommendations of the machine, tooling, and coolant manufacturers.
Maintain Consistent Delivery
Interrupted or inconsistent coolant flow can lead to unstable machining conditions. Coolant systems should therefore be inspected regularly to ensure pumps, filters, nozzles, and lines are working correctly.
Coolant Maintenance in CNC Machining
Coolant quality can deteriorate over time. Contamination, incorrect concentration, bacterial growth, tramp oil, chips, and other contaminants can reduce coolant effectiveness.
A proper maintenance routine should include:
- Checking coolant concentration
- Removing chips and debris
- Monitoring contamination
- Inspecting coolant levels
- Cleaning filters
- Checking pumps and delivery lines
- Monitoring fluid condition
- Maintaining appropriate fluid concentration
- Following the coolant manufacturer's maintenance recommendations
Regular monitoring helps maintain consistent machining conditions and can also improve workplace cleanliness.
Common Coolant Mistakes to Avoid
Several common mistakes can reduce the benefits of coolant.
Using the Wrong Concentration
An incorrect coolant concentration can affect lubrication, cooling, corrosion protection, and fluid stability.
The concentration should be checked using the appropriate method recommended by the coolant manufacturer.
Poor Nozzle Positioning
If coolant does not reach the cutting zone, much of its potential benefit is lost.
Nozzle positioning should be checked whenever tools, fixtures, or workholding arrangements change.
Neglecting Coolant Maintenance
Old or contaminated coolant may cause unpleasant odors, corrosion, poor machining performance, and other operational problems.
Regular inspection and maintenance are essential.
Changing Between Wet and Dry Machining Without Considering Tool Requirements
Some cutting tools and operations are designed for dry machining, while others benefit from coolant. Switching conditions without considering the tool manufacturer's recommendations can create thermal or performance problems.
Coolant and Different CNC Machining Tools
Proper coolant use should be considered alongside overall tooling strategy.
CNC machining tools such as drills, end mills, turning inserts, reamers, grooving tools, and threading tools can all have different coolant requirements.
For example, drilling may require strong chip evacuation, while milling may require carefully controlled coolant application depending on the tool geometry and cutting conditions.
Similarly, machining accessories, tool holders, workholding systems, and coolant delivery equipment should work together to create a stable machining setup.
How Proper Coolant Use Improves Productivity
The benefits of coolant extend beyond tool life.
Effective coolant management can contribute to:
- Longer cutting tool service life
- More consistent machining performance
- Improved surface finish
- Better chip evacuation
- Reduced heat generation
- Lower risk of certain tool failures
- More stable dimensional accuracy
- Reduced unplanned tool changes
- Improved machine productivity
- More predictable production costs
However, coolant is not a substitute for correct tool selection or machining parameters. Tool geometry, cutting speed, feed rate, workholding, machine rigidity, and tool condition must all be considered together.
Best Practices for Coolant Use
Workshops can improve coolant performance by following a practical checklist:
- Select coolant according to the material and machining operation.
- Follow the recommended coolant concentration.
- Position nozzles toward the actual cutting zone.
- Maintain adequate coolant flow and pressure.
- Keep coolant systems clean.
- Remove chips and contamination regularly.
- Monitor fluid condition and concentration.
- Inspect pumps, filters, hoses, and nozzles.
- Follow tooling manufacturer's coolant recommendations.
- Monitor cutting tool wear and adjust machining conditions when necessary.
These practices can help create more predictable machining results.
The Role of Tool Selection and Measurement
Coolant management works best when combined with appropriate tooling and measurement practices.
High-quality industrial cutting tools must be matched to the workpiece material and operation. Proper CNC tool holders should provide rigidity and minimize unnecessary runout or vibration.
After machining, precision measuring tools can be used to verify critical dimensions and identify whether tool wear or thermal effects are affecting production quality.
This combination of proper tooling, coolant management, machine setup, and measurement creates a more controlled machining process.
Conclusion
Proper coolant use plays an important role in controlling heat, reducing friction, improving chip evacuation, protecting surface finish, and supporting longer cutting tool life. However, the best results come from treating coolant as one part of a complete machining strategy.
Workpiece material, cutting tool material, geometry, cutting parameters, machine rigidity, tool holding, coolant type, delivery method, and maintenance should all be considered together.
For companies seeking reliable industrial tooling solutions, Khokhawala Trading LLC offers a broad selection of industrial cutting tools, carbide cutting tools, CNC machining tools, machining accessories, and precision measuring tools for demanding industrial applications. As an experienced Industrial Tools Supplier in Dubai, Khokhawala Trading LLC supports workshops and businesses looking to improve machining efficiency, consistency, and tool performance.
With the right coolant strategy and properly selected tooling, manufacturers can create more stable machining conditions, reduce avoidable tool wear, and achieve reliable production results.
0 comments
Log in to leave a comment.
Be the first to comment.