
How a Shot Blasting Machine Improves Metal Surface Finish
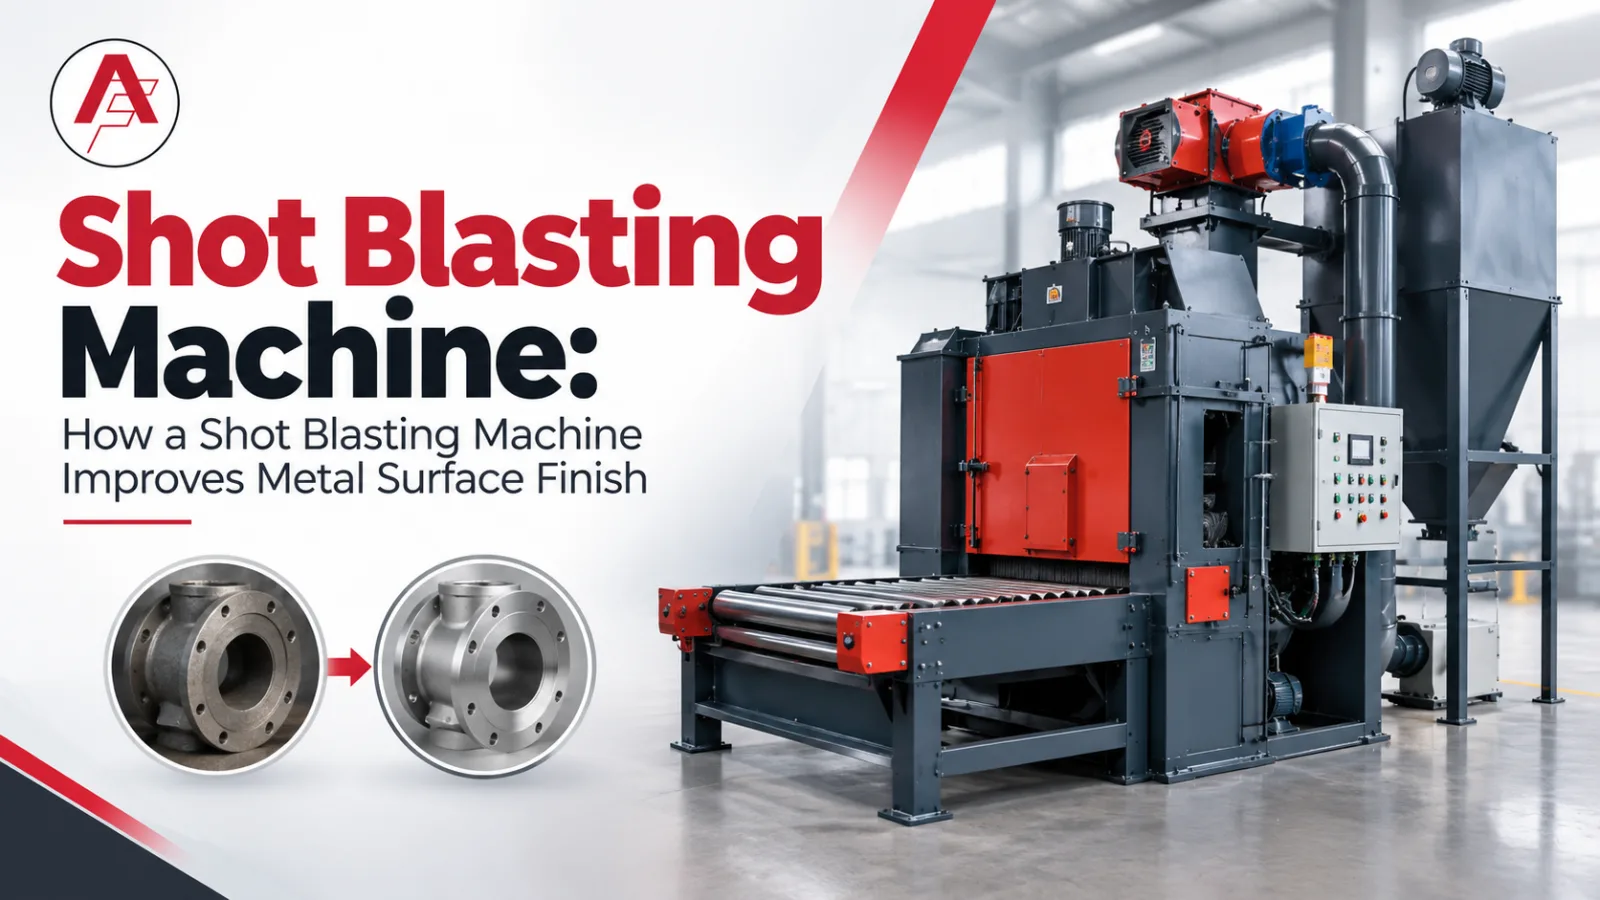
Quick Summary: A shot blasting machine throws small steel particles at a metal surface at high speed to remove rust, scale and old coating, and to leave a clean, even texture. This improves paint adhesion, appearance and part life. The result depends on the type of abrasive, its size, the machine type and the blasting time. This guide explains how it works and how to get the finish you want.This article explains how it works, how it improves surface finish, the main machine types, how to choose one and how to keep it running well.
Why Surface Finish Matters
Think about a freshly cast or fabricated metal part. It rarely looks the way you want. There may be a crust of mill scale, patches of rust, sand stuck from the mould, weld spatter or old paint. If you coat it without cleaning, the paint peels in a few months. If you machine it without cleaning, tools wear faster.Surface finish is not only about looks. It decides how well coatings stick, how well a part resists corrosion and wear, and sometimes how long it lasts under repeated stress. A poor surface causes rework, rejections and complaints, and a good one saves all three.That is why so many factories use shot blasting as a standard step before painting, plating or machining.
What Is a Shot Blasting Machine?A shot blasting machine is an industrial machine that uses a stream of abrasive particles, such as steel shot or steel grit, to clean and finish the surface of metal parts. In the most common design, high-speed wheels throw the abrasive onto the part inside an enclosed cabinet or chamber. The abrasive falls back, is cleaned and is reused again and again.
It is used on castings, forgings, fabricated structures, plates, tubes, springs and many other parts. Some machines also work on concrete and other materials.
How It Improves Metal Surface FinishShot blasting improves the surface in several ways at once.
Types of Shot Blasting MachinesThe right machine depends on what you blast.
Most machines include a dust collector, an abrasive cleaning and recycling system, and safety interlocks.
What Controls the Final Finish?To get a repeatable finish, you control a few key settings.
It helps to write down the settings that give a good result for each part type, and to repeat them each time.
Common Finish Problems and Fixes
How to Choose the Right MachineStart from your parts, not from the catalogue.
Sharing sample parts with the manufacturer is one of the best ways to get a good recommendation.
Maintenance Tips
Final ThoughtsGood surface finish is a quiet advantage. It shows up as paint that lasts, parts that fit and customers who do not send things back. A shot blasting machine delivers that finish quickly and consistently. Choose the machine to match your parts, pick the right abrasive and keep the settings and maintenance under control.If you would like to see what a modern shot blasting machine range looks like, you can explore the models offered by Adarsh Fabricators, which include airblast, wheelblast and tumblast designs for rust and scale removal, paint removal and surface preparation.
Frequently Asked Questions
Q. What is a shot blasting machine used for?Ans. It is used to clean, descale, deburr and prepare metal surfaces by blasting them with abrasive particles such as steel shot or grit.
Q. How does shot blasting improve surface finish?Ans. It removes rust, scale and old coatings, and leaves a clean, uniform, slightly textured surface. This improves coating adhesion and hides small surface flaws.
Q. What is the difference between shot and grit?Ans. Shot is round and gives a smoother, peened surface. Grit is angular and cuts deeper, giving a rougher profile and faster cleaning.
Q. What are the types of shot blasting machines?Ans. Common types are tumble belt, hanger type, table, roller conveyor and air blast machines. The right one depends on the size and shape of your parts.
Q. Is shot blasting the same as shot peening?Ans. No. Shot peening is a controlled process that treats the surface to improve fatigue strength. Ordinary shot blasting mainly cleans and prepares the surface, though it can add a mild peening effect.
Q. Can shot blasting damage metal parts?Ans. If the abrasive is too large or the exposure too long, it can roughen or distort thin parts. The right settings prevent this.
Q. What materials can be shot blasted?Ans. Steel, cast iron and many other metals can be blasted. Some machines also treat concrete and other materials. The abrasive and the settings should suit the material.
Q. Why should coating be done soon after shot blasting?Ans. Blasted steel is clean and active, so it can start to rust quickly. Coating soon after blasting gives the best protection and adhesion.
Why Surface Finish Matters
Think about a freshly cast or fabricated metal part. It rarely looks the way you want. There may be a crust of mill scale, patches of rust, sand stuck from the mould, weld spatter or old paint. If you coat it without cleaning, the paint peels in a few months. If you machine it without cleaning, tools wear faster.Surface finish is not only about looks. It decides how well coatings stick, how well a part resists corrosion and wear, and sometimes how long it lasts under repeated stress. A poor surface causes rework, rejections and complaints, and a good one saves all three.That is why so many factories use shot blasting as a standard step before painting, plating or machining.
What Is a Shot Blasting Machine?A shot blasting machine is an industrial machine that uses a stream of abrasive particles, such as steel shot or steel grit, to clean and finish the surface of metal parts. In the most common design, high-speed wheels throw the abrasive onto the part inside an enclosed cabinet or chamber. The abrasive falls back, is cleaned and is reused again and again.
It is used on castings, forgings, fabricated structures, plates, tubes, springs and many other parts. Some machines also work on concrete and other materials.
How It Improves Metal Surface FinishShot blasting improves the surface in several ways at once.
- It removes contamination. Rust, mill scale, sand, weld spatter and old coatings are knocked off by the repeated impact.
- It cleans to a consistent level. Machines can reach a thorough cleaning level, often described as Sa 2.5 under the ISO 8501-1 standard, in a repeatable way.
- It creates a uniform texture. The surface becomes evenly matt, which hides small marks and tool lines.
- It makes a profile for coatings. The tiny peaks and valleys give paint, powder coat or plating something to grip. This is often called the anchor pattern.
- It can remove burrs and fins. Light burrs and flash on cast or forged parts get knocked away.
- It adds a peening effect. The impact can compress the surface layer, which may improve resistance to fatigue and cracking. Note that controlled shot peening is a separate, precise process, but ordinary blasting can still give a mild benefit.
- It saves time. One machine can treat large batches faster and more evenly than hand tools like wire brushes and grinders.
- The result is a part that is ready for the next step, with fewer defects and fewer surprises.
- Shot vs Grit: What Changes the Finish?
- The abrasive you choose has a big effect on the surface.
- Steel shot is round. It peens the surface, gives a smoother, more uniform matt finish and is gentler on the part. It is often used for cleaning, light descaling and peening.
- Steel grit is angular and sharp. It cuts the surface, gives a rougher, deeper profile and removes heavy scale and rust faster.
- A mix of shot and grit gives a balance of cleaning speed and finish. Many plants use a working mix that they top up regularly.
- Particle size matters too. Larger particles hit harder and create a rougher surface. Smaller particles give a finer finish. The hardness of the abrasive and the hardness of the part also play a role.
Types of Shot Blasting MachinesThe right machine depends on what you blast.
- Tumble belt machines: parts tumble on a rubber belt while being blasted. Good for small, tough parts in bulk, such as small castings and forgings.
- Hanger type machines: larger parts hang on hooks and rotate in the blast stream. Good for medium to heavy castings and fabrications.
- Table or turntable machines: parts sit on a rotating table. Good for medium and flat items.
- Roller conveyor or pass-through machines: long parts such as plates, beams and pipes move through the blast chamber. Common in structural steel and shipyards.
- Air blast machines: use compressed air to propel the abrasive. They suit small parts, detailed work and spot treatment.
Most machines include a dust collector, an abrasive cleaning and recycling system, and safety interlocks.
What Controls the Final Finish?To get a repeatable finish, you control a few key settings.
- Abrasive type and size: the biggest influence on texture.
- Wheel speed or blast pressure: higher energy means a rougher, faster result.
- Exposure time: longer blasting gives a more thorough and more textured surface.
- Abrasive flow rate: the right amount of abrasive keeps the blast steady.
- Part position and movement: parts must turn or travel so that every area is covered.
- Abrasive condition: worn, broken or dirty abrasive gives poor results.
- Cleanliness of the abrasive mix: oil, dust and moisture affect the finish.
It helps to write down the settings that give a good result for each part type, and to repeat them each time.
Common Finish Problems and Fixes
- Uneven finish or shadow areas: parts may be shielded from the blast. Change the loading pattern, or the way the parts rotate.
- Surface too rough: reduce the abrasive size, switch to more shot than grit, or shorten the blasting time.
- Not clean enough: increase the time, use sharper grit or check the wheel speed.
- Distortion of thin parts: the impact may be too strong. Use smaller, lighter shot, and a shorter time.
- Rust returning quickly: blasted steel is very reactive. Coat or protect the parts soon after blasting.
- Dust or oil contamination: clean the abrasive and the machine regularly.
- Worn parts in the machine: worn blades and liners reduce performance and change the blast pattern.
How to Choose the Right MachineStart from your parts, not from the catalogue.
- Part size, weight and shape: this decides the machine type and chamber size.
- Production volume: how many parts per hour or per shift.
- Finish required: the cleanliness level, the profile and the look you need.
- Material: cast iron, steel, aluminium and other metals need different abrasives.
- Loading method: manual, conveyor or automatic.
- Dust control and environment: a proper dust collector protects workers and the plant.
- Safety features: interlocks, guards and clear controls.
- Build quality and wear parts: strong construction and easy access for replacement.
- Service support: spares, training and installation.
Sharing sample parts with the manufacturer is one of the best ways to get a good recommendation.
Maintenance Tips
- Check the blast wheel blades, liners and control cage on a fixed schedule.
- Keep the abrasive mix topped up and well graded.
- Clean the dust collector and the separator regularly.
- Keep the abrasive dry.
- Lubricate the bearings and moving parts as advised.
- Inspect door seals and safety interlocks.
- Keep a record of wear part life, abrasive use and downtime.
Final ThoughtsGood surface finish is a quiet advantage. It shows up as paint that lasts, parts that fit and customers who do not send things back. A shot blasting machine delivers that finish quickly and consistently. Choose the machine to match your parts, pick the right abrasive and keep the settings and maintenance under control.If you would like to see what a modern shot blasting machine range looks like, you can explore the models offered by Adarsh Fabricators, which include airblast, wheelblast and tumblast designs for rust and scale removal, paint removal and surface preparation.
Frequently Asked Questions
Q. What is a shot blasting machine used for?Ans. It is used to clean, descale, deburr and prepare metal surfaces by blasting them with abrasive particles such as steel shot or grit.
Q. How does shot blasting improve surface finish?Ans. It removes rust, scale and old coatings, and leaves a clean, uniform, slightly textured surface. This improves coating adhesion and hides small surface flaws.
Q. What is the difference between shot and grit?Ans. Shot is round and gives a smoother, peened surface. Grit is angular and cuts deeper, giving a rougher profile and faster cleaning.
Q. What are the types of shot blasting machines?Ans. Common types are tumble belt, hanger type, table, roller conveyor and air blast machines. The right one depends on the size and shape of your parts.
Q. Is shot blasting the same as shot peening?Ans. No. Shot peening is a controlled process that treats the surface to improve fatigue strength. Ordinary shot blasting mainly cleans and prepares the surface, though it can add a mild peening effect.
Q. Can shot blasting damage metal parts?Ans. If the abrasive is too large or the exposure too long, it can roughen or distort thin parts. The right settings prevent this.
Q. What materials can be shot blasted?Ans. Steel, cast iron and many other metals can be blasted. Some machines also treat concrete and other materials. The abrasive and the settings should suit the material.
Q. Why should coating be done soon after shot blasting?Ans. Blasted steel is clean and active, so it can start to rust quickly. Coating soon after blasting gives the best protection and adhesion.
0 comments
Log in to leave a comment.
Be the first to comment.