
How a Hydraulic Foam Cutting Machine Improves Industrial Cutting Efficiency
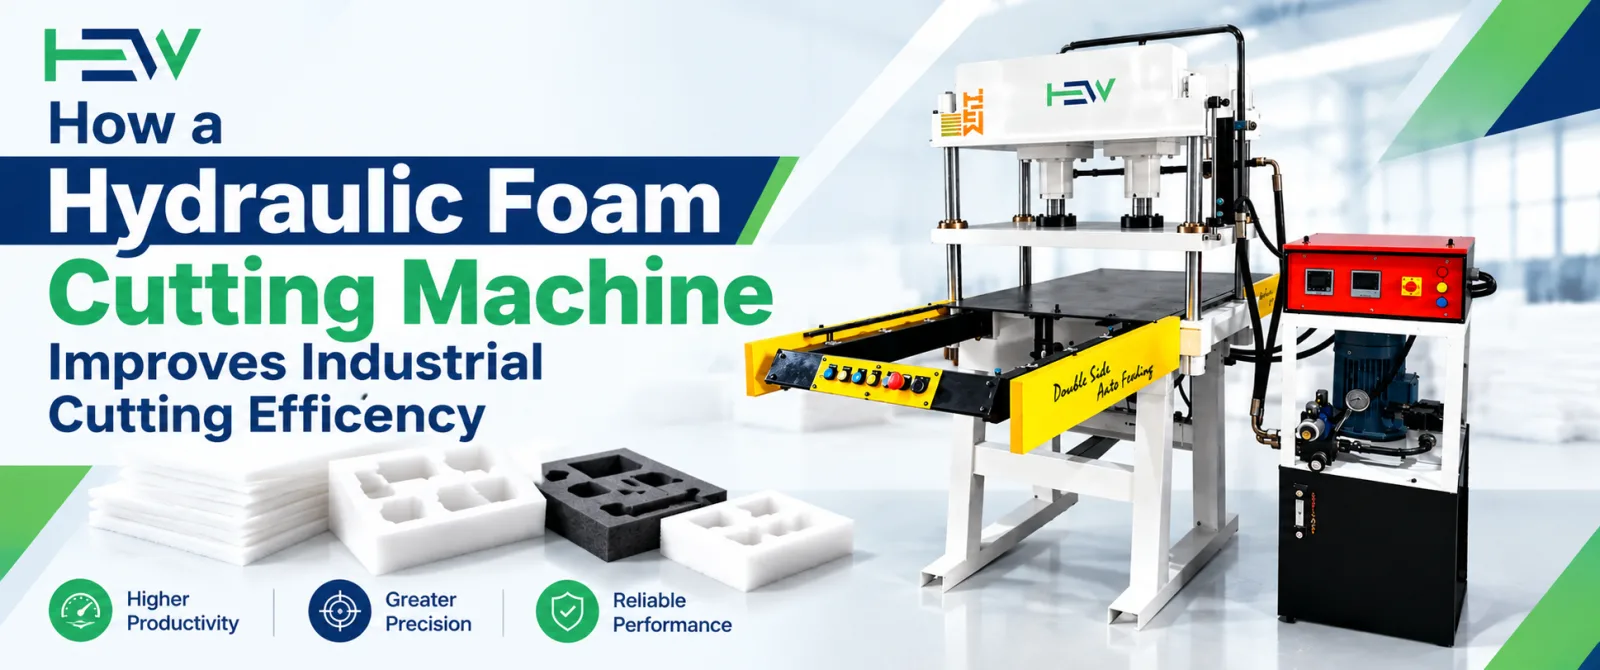
A hydraulic press forces a steel die through foam with controlled, repeatable pressure. That gives matching pieces, stack cutting, tight layouts, and quick die changes. This article explains how the hydraulic foam cutting machine works, where the efficiency gains come from, how it compares with CNC and manual cutting, what to check before buying, and how to avoid common setup and maintenance mistakes.
Introduction
Every foam plant has some leaking points somewhere on the cutting floor. It is because maybe the operators mark and trim each piece by eye, or the top layer of a stack matches the drawing while the bottom one drifts, or it might be too much of the sheet ends up in the scrap bin. A hydraulic foam cutting machine plugs those leaks one stroke at a time. A die fixes the shape, steady hydraulic force carries it through the foam, and the result repeats cut after cut. Mattress makers, upholstery units, packaging lines, and automotive seat suppliers lean on this approach because it saves time on every single piece and foam on every sheet. In the sections below, we'll trace where cutting time is lost, how the machine recovers it, which materials and industries benefit most, and what to check before you buy. Read on, and you'll know how to decide whether it deserves a place on your line.
Common Problems in Foam Cutting
Before you judge any machine, look at where the time went today. On most foam floors the cut itself takes seconds. The rest disappears into marking, measuring, trimming, re-cutting, and carrying rejects to a pile. Nobody times those minutes, so nobody sees them.
Quality drifts in different ways too. Without a hydraulic foam cutting machine, a hand cut piece that runs a few millimetres small still reaches the sewing table or the packing bench. Then it causes a wrinkle in an upholstered cover or a rattle inside a carton. Scrap is the third leak. Foam is a major material cost in plants like these, and loose layouts waste it sheet after sheet.
How a Hydraulic Foam Cutting Machine Helps Saves Time
Each loss above has a matching fix inside the machine. This is how the machine saves time:
1. One Die Defines Every Part
A steel rule die carries the shape, so nobody measures or marks. The operator places the sheet, brings the cutting head down, and the part leaves with the same size and profile as the one before it. The die, not the operator, becomes the tolerance, and rework drops with it.
2. Top Layer and Bottom Layer Stay Matched
Stacked cutting on a hydraulic foam cutting machine multiplies output per stroke, but only if the bottom layer matches the top. HEW builds its machines to cut layers together without size differences between the uppermost and lowermost sheet. Even so, test your own foam first, because density and thickness decide how tall a stack you can run.
3. Smarter Layouts Mean Less Waste
A die layout decides how much foam leaves as parts and how much leaves as offcuts. Nest the dies tightly, turn irregular shapes so they share edges, and send offcuts to smaller parts where you can. An hour at the layout table saves foam on every sheet that follows.
4. Less Strain on Operators
Placing, cutting, and removing is easier on hands and eyes than hours of knife work. Operators hold a steadier pace across the shift, and quality stops depending on who feels tired.
Why Steady Hydraulic Force Suits Soft Material
Mechanical presses drive the die with a flywheel and crank. They run quickly, but the stroke is fixed and the force peaks near the bottom. A hydraulic foam cutting machine delivers steady force through the stroke, and you can set its travel and pressure for each working condition. HEW lists adjustable cutting thickness among its features.
Soft foam rewards that control. Thin packaging foam and thick cushion foam need different settings, and the right depth lets the blade slice through instead of crushing the edge. You may give up a little speed per stroke. You gain control over every cut.
Industries and Materials That Gain Most
Plenty of plants already run this way. Mattress and sofa makers cut cores and panels. Automotive seat suppliers cut cushions and trim layers. Packaging lines punch EPE foam inserts. Soundproofing, medical foam products, and construction or interior panels follow the same logic.
The material range is wide too. PU foam, EVA foam, EPE foam, and sponge all cut well, and HEW says its machines also handle leather, film, and fabric in sheet or roll form. Denser material needs more force and sharper dies, so size the machine for your toughest working conditions, not your average one.
Press, Band Knife, or CNC Knife: Matching the Tool to the Work
Different tools win on different work:
Repeat the same shapes in volume and the die cost spreads thinly over thousands of parts. Change shapes daily and a CNC knife spares you the die bill. Many plants keep both.
What to Ask Before You Order
Ask the supplier these questions before buying a hydraulic foam cutting machine:
Which force and table size suit my largest die and thickest foam?
Do you offer manual and automatic operation, and which fits my volume?
Can I adjust cutting thickness for each cutting work?
Which safety features come standard?
How fast can I get dies, cutting boards, and spares?
We list single side, double side, and manual foam punching machines, so describe your daily output and foam type and let the supplier narrow the choice. Bring sample foam to a trial if you can.
Habits That Keep a Cutting Line Smooth
Most breakdowns on a hydraulic foam cutting machine start with small neglect. Dull dies at the top of the list. Operators raise pressure to compensate, and the board and cylinder pay for it. Sharpen or replace the die instead.
The cutting board comes next. It wears into grooves, cuts stop going through, and people blame the foam. Rotate or resurface the board early.
Then comes routine care. Check hydraulic oil and hoses on the supplier's schedule, sweep foam dust off the table each shift, and store dies flat with their edges protected. Keep a log of settings for different working conditions, so a new operator starts from proven numbers. These steps cost minutes and prevent long stoppages.
Conclusion
Efficiency on a foam line rarely comes from one big change. It comes from removing small losses: the marking, the rework, the drifting layers, the scrap. A hydraulic foam cutting machine takes care of all four when you match it to your material and look after it. The HEW Foam Cut Machine can walk you through the options for your foam type, sheet size, and daily volume, so you choose a machine that earns its place from the very first shift.
FAQs
Q. What does a hydraulic foam cutting machine do?
This foam cutting machine is used to cut or punch sheet foam and similar soft material into identical shapes using a steel rule die and steady hydraulic force.
Q. Which foams and materials can it cut?
A hydraulic foam cutting machine can easily cut PU foam, EVA foam, EPE foam, and sponge are common. HEW also lists leather, film, and fabric. Check the machine's rating against your thickest, densest material.
Q. Should I buy a press or a CNC foam cutter?
The decision from these two completely depends on the type of material you are cutting. Buy a press for volume work with repeating shapes. Choose CNC when designs change often and runs stay short. Some plants run both.
Q. How many layers can I cut in one stroke?
The number of layers this hydraulic foam cutting machine can cut completely depends on foam type, thickness, die size, and machine force. Run a trial and check the bottom layer, since it shows trouble first.
Q. How often should I change the cutting board?
There is no fixed time limit in which you should change the cutting board. Rotate or resurface it before grooves form, and replace it when cuts stop going through cleanly.
Q. Do operators need training?
Yes, a short course is important for every trainer. Operators should learn the controls, safety devices, die changes, and your plant's safety rules before they run production.
0 comments
Log in to leave a comment.
Be the first to comment.