
Food Conveyors: Types, Benefits, and How to Choose the Right System
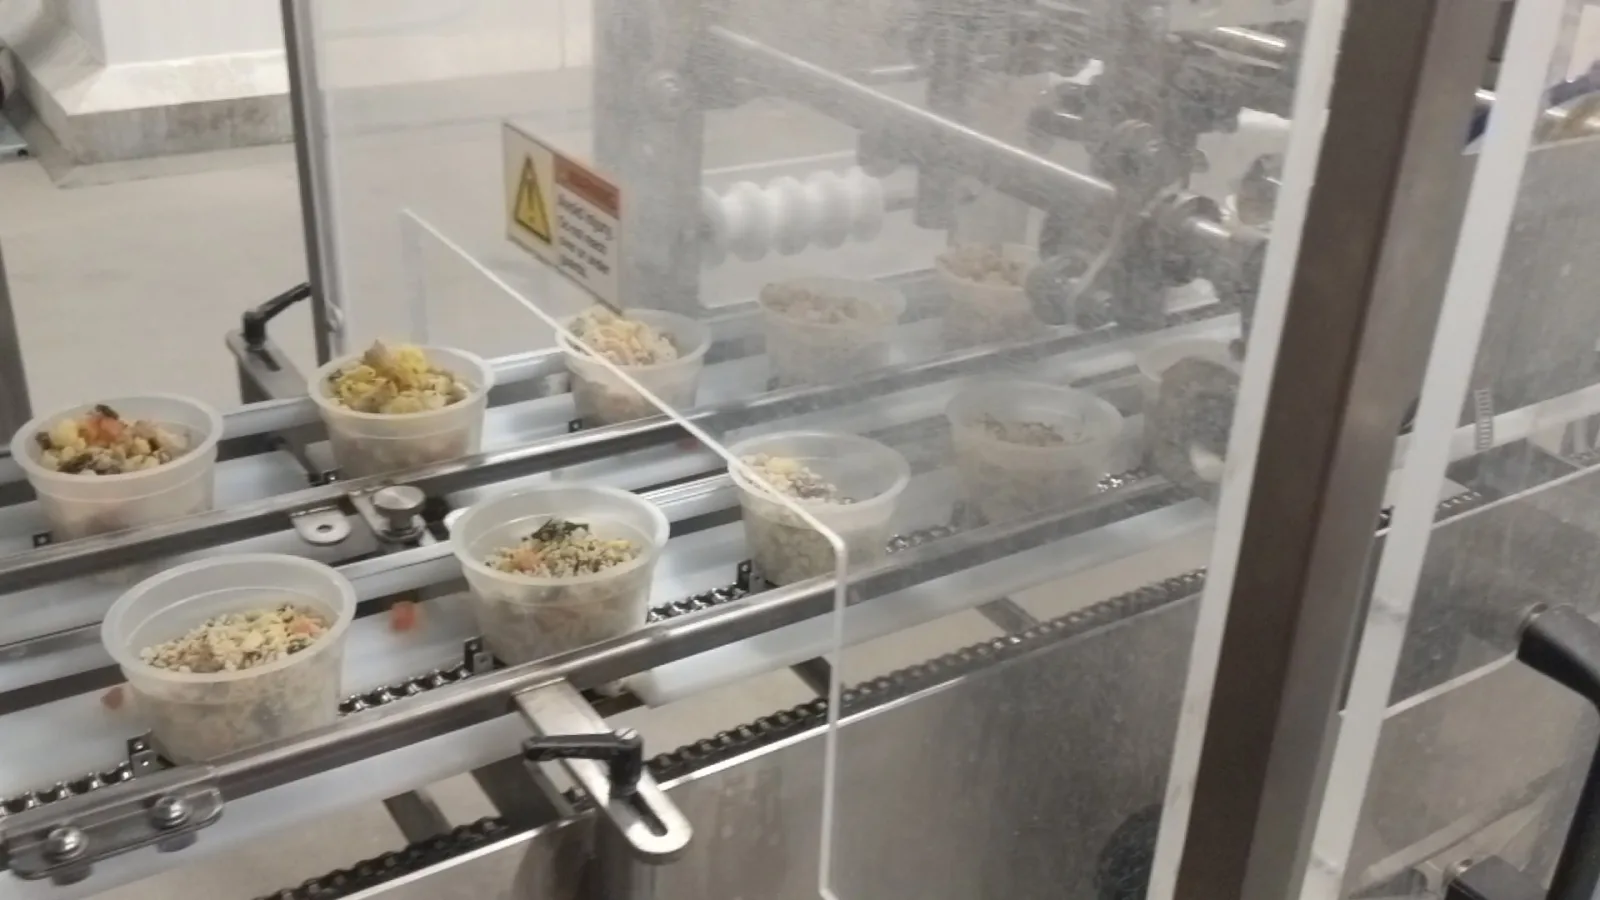
Every food plant has one thing in common: product is always on the move. Ingredients travel to mixers, dough heads to ovens, and packaged goods roll toward shipping. Food conveyors connect each of those steps, and the right system keeps production steady while supporting sanitation.
This guide explains the main types of food conveyors, what they do well, and what to check before you choose one.
What Are Food Conveyors?
Food conveyors are material handling systems built to move ingredients, partly finished items, and packaged goods through a food plant. Unlike general industrial conveyors, they are designed for frequent washdown and clean operation.
Common design features include stainless steel frames, open construction, and smooth surfaces. These details make cleaning easier and help limit places where residue can collect.
Types of Food Conveyors
Most plants use more than one conveyor style. The best mix depends on what you move and where it needs to go. For a deeper look, see this overview of the types of conveyors used in the food industry.
Chain Conveyors
Chain conveyors use chains fitted with paddles or scrapers to push bulk material through a trough or tube. They suit gentle handling of fine materials.
Screw Conveyors
A screw conveyor moves bulk material with a rotating helical blade. Speed and pitch can be adjusted to control flow, which makes them useful for grains, powders, and ingredient feeding. You can read more about screw conveyors.
Z-Conveyors and Bucket Conveyors
These lift product vertically and save floor space. They help when a line needs to change levels.
Spiral Conveyors
Spiral conveyors move product between levels in a continuous flow. They work well in high-volume plants with limited space.
Metal Detector and Weigh-Station Conveyors
Metal detector conveyors carry product past a detector and reject contaminated items. Weigh-station conveyors check weight as product moves, which supports accurate packaging.
Specialty Conveyors
Vibrating, screen, slat, retractable nose, and vacuum conveyors solve more specific needs, such as gentle handling, sorting by size, moving heavy items, or reducing dust.
Benefits of Food Conveyors
Good conveyor planning pays off in everyday ways.
- Smoother product flow: Fewer stops between process steps.
- Less manual handling: Workers lift and carry less, which lowers strain.
- Faster cleaning: Food grade, open designs can shorten washdown time.
- Better food safety: Enclosed transfer and metal detection help protect product quality.
- Flexible layouts: Vertical, curved, and spiral designs fit real floor plans.
How to Choose Food Conveyors for Your Plant
Start with your product, your space, and your sanitation routine. Then ask these questions:
- Is the product dry, wet, sticky, fragile, or frozen?
- How much do you need to move per hour?
- How much floor and overhead space is available?
- How often will the conveyor be washed down, and with what method?
- What equipment will it connect to?
If your layout is complex, a custom design may fit better than a standard model. Some builders, including CHL Systems, offer conveyance and process improvement services that cover planning through installation.
Final Thoughts
Food conveyors shape how smoothly a plant runs, how easy it is to clean, and how safely product is handled. Match the conveyor type to your product and process, and choose a supplier with real food industry experience. To talk through your project, you can contact CHL Systems.
Frequently Asked Questions
What Types of Conveyors Are Used in the Food Industry?
Common types include chain, screw, Z and bucket, spiral, metal detector, weigh-station, vibrating, screen, slat, retractable nose, and vacuum conveyors. The right choice depends on the product and the process.
What Are the Four Main Types of Conveyors?
Conveyors are often grouped into belt, roller, chain, and screw types, although sources sometimes list them differently. In food plants, these basic styles are adapted with sanitary materials and open designs.
Who Are the Largest Food Processing Equipment Manufacturers in the USA?
There is no single official ranking, and size depends on whether you measure revenue, product range, or a specific equipment category. It is better to compare suppliers by food industry experience, sanitary design, custom engineering, and service support.
What Are the Major Conveyor Companies in the USA?
The market includes many large manufacturers and smaller specialists. Rather than relying on a list, review each company’s experience in food plants, the equipment it builds, and the installation and parts support it offers.
0 comments
Log in to leave a comment.
Be the first to comment.