
Dual FBE Coating: Advanced Protection for Long-Lasting Industrial Pipeline Performance

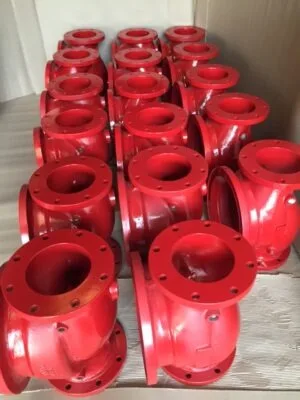
Industrial pipelines and metal surfaces are constantly exposed to moisture, chemicals, soil conditions, and other environmental factors that can cause corrosion. Protecting these surfaces is essential for maintaining their strength, performance, and service life. Dual FBE coating is an effective protective solution designed to provide enhanced corrosion resistance and long-term durability in demanding industrial environments.
Dual FBE (Fusion Bonded Epoxy) coating uses two layers of epoxy material to create a strong protective barrier over metal surfaces. This coating system is widely used in pipeline applications where reliable protection against corrosion, mechanical damage, and environmental exposure is important. It helps industries maintain the quality of their infrastructure while reducing maintenance requirements.
Understanding Dual FBE Coating
Dual FBE coating is a specialized coating system that consists of two functional epoxy layers applied to a properly prepared metal surface. The first layer provides strong adhesion and corrosion protection, while the second layer adds extra thickness and improves resistance to mechanical stress. Together, these layers create a durable coating that helps protect pipelines from external damage.
The coating process generally involves surface preparation, controlled heating, and the application of epoxy powder. Once the powder comes into contact with the heated metal surface, it melts and forms a continuous protective film. Proper application and curing are important for achieving consistent coating quality.
Importance of Dual FBE Coating in Industrial Applications
Corrosion can gradually weaken metal pipelines and affect their operational efficiency. In industries such as oil and gas, water distribution, petrochemicals, and infrastructure development, pipeline protection plays an important role in maintaining safe and reliable operations.
Dual FBE coating provides an additional level of protection compared to conventional single-layer coating systems. Its two-layer structure helps improve coating performance in challenging conditions. It also offers excellent adhesion, making it suitable for applications where pipelines remain buried underground or operate in environments with changing temperatures and moisture levels.
Another important advantage is its ability to create a uniform protective layer. When applied using appropriate procedures, the coating covers the metal surface effectively and helps reduce the chances of corrosion-related deterioration.
Key Benefits of Dual FBE Coating
There are several reasons why industries choose dual-layer fusion bonded epoxy systems for pipeline protection.
-
Enhanced Corrosion Resistance: The epoxy layers create a protective barrier that reduces direct contact between metal surfaces and corrosive elements.
-
Strong Adhesion: The coating bonds firmly with properly prepared steel, helping maintain its protective performance.
-
Improved Mechanical Protection: The additional layer provides greater coating thickness and helps resist handling and installation-related damage.
-
Long-Term Durability: It supports extended pipeline service life by protecting surfaces from environmental exposure.
-
Chemical Resistance: The coating can withstand exposure to many industrial substances, depending on the formulation and operating conditions.
-
Reduced Maintenance: Effective corrosion protection can help minimize the need for frequent repairs and coating replacement.
Understanding the Dual FBE Coating Service Process
A professional Dual FBE Coating Service involves several important steps to ensure that the finished coating meets the required quality standards. The process begins with careful inspection of the metal surface to identify rust, oil, dust, and other contaminants.
The next step is abrasive blasting, which removes unwanted materials and creates a suitable surface profile for epoxy adhesion. Cleanliness is essential because contaminants can affect the bonding strength and overall coating performance.
After surface preparation, the steel component is heated to the specified temperature. The first layer of fusion bonded epoxy powder is then applied to provide corrosion protection and strong adhesion. A second layer is applied according to the required coating specifications to improve overall thickness and mechanical performance.
The coated material is allowed to cure under controlled conditions. Finally, quality inspections are performed to evaluate coating thickness, appearance, adhesion, and other relevant properties. Holiday testing may also be conducted to identify small gaps or defects in the protective layer.
Applications of Dual FBE Coating
Dual FBE coating is suitable for several industrial applications where metal protection is a priority. It is commonly used for oil and gas transmission pipelines, underground water pipelines, industrial processing systems, and infrastructure projects.
It can also be used in applications involving steel pipes that require additional protection during transportation, storage, and installation. Its performance makes it a valuable option for projects where corrosion resistance and coating durability are important considerations.
The selection of a suitable coating system depends on factors such as pipeline diameter, operating temperature, environmental exposure, installation conditions, and project specifications.
Why Choose Heatman Products for Dual FBE Coating Solutions?
Choosing the right coating provider is important for achieving reliable industrial protection. Heatman Products focuses on delivering coating solutions designed to meet different industrial requirements. Understanding surface preparation, coating materials, application procedures, and quality control is essential for producing consistent results.
Heatman Products recognizes the importance of durable coating systems for protecting industrial infrastructure. Its approach emphasizes proper application practices and attention to coating quality. Whether a project requires corrosion protection for pipelines or additional surface durability, selecting an appropriate coating system can make a significant difference in long-term performance.
Conclusion
Dual FBE coating is a reliable solution for improving the corrosion resistance and durability of industrial pipelines and steel surfaces. Its two-layer structure provides strong adhesion, additional coating thickness, and protection against challenging environmental conditions. A professionally delivered Dual FBE Coating Service helps ensure proper surface preparation, uniform application, and consistent coating quality.
With suitable coating selection and application practices, industries can protect valuable pipeline infrastructure, reduce maintenance concerns, and support long-term operational efficiency. Heatman Products aims to provide dependable coating solutions that address the changing protection needs of modern industrial applications.
0 comments
Log in to leave a comment.
Be the first to comment.