
Complete Guide to Choosing a Commercial RO Plant Manufacturer in Noida
Commercial RO Plant Manufacturer in Noida
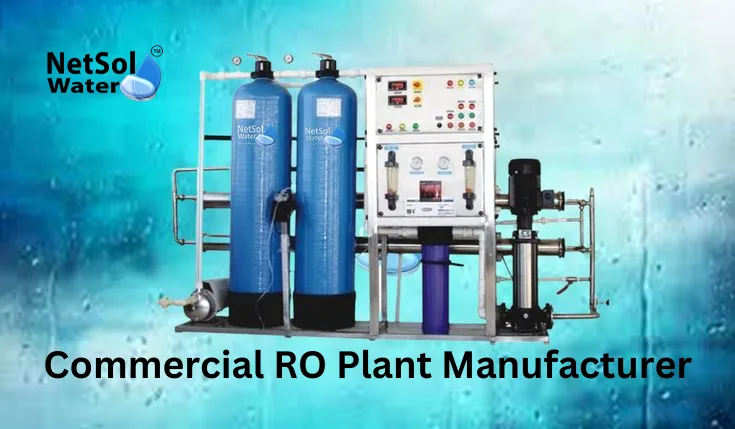
Finding the right commercial RO plant manufacturer in Noida is an important decision for any business that depends on a steady supply of purified water. Hotels, hospitals, restaurants, schools, offices, housing projects and manufacturing facilities may all have different water requirements. Because of this, choosing an RO plant should never be based only on price or plant capacity.
A properly designed commercial RO system can help control dissolved salts and other unwanted substances in feed water. However, its performance depends on several factors. These include the quality of the source water, required output, pretreatment, membrane selection, recovery rate, operating pressure and regular maintenance.
Noida has a wide mix of commercial and industrial establishments. As a result, businesses often need water treatment systems designed around their actual site conditions. This guide explains what you should look for when selecting an RO plant manufacturer and how to avoid common mistakes.
Why Do Businesses in Noida Need Commercial RO Plants?
Water quality can vary considerably from one location to another. A business may receive water from a municipal source, borewell or another supply. The water may contain dissolved salts, hardness, suspended particles or other impurities.
A commercial RO plant can reduce many dissolved contaminants through a semi-permeable membrane. The system separates treated water from a concentrated reject stream. Therefore, the complete plant needs to be designed around both the required product water and the feed-water characteristics.
Businesses may use RO-treated water for several purposes, such as:
- Drinking water
- Food and beverage operations
- Hotels and restaurants
- Schools and educational institutions
- Hospitals and healthcare facilities
- Office buildings
- Process applications
- Boiler feed pretreatment
- Equipment and cleaning applications
The required water quality can differ for every application. So, the first step should always be understanding how you plan to use the treated water.
Start With a Detailed Water Analysis
One of the biggest mistakes businesses make is selecting an RO plant before testing their feed water.
A good manufacturer should first understand the water entering the system. A water analysis can provide information about parameters such as:
- TDS
- pH
- Hardness
- Turbidity
- Alkalinity
- Iron
- Chloride
- Sulphate
- Silica
- Microbiological parameters where relevant
The exact testing requirements depend on the water source and application.
Why does this matter?
Because RO membranes do not work in isolation. If the feed water contains high levels of suspended solids or hardness, suitable pretreatment may be required. Without proper pretreatment, membranes can foul or scale faster.
Therefore, choose a manufacturer that treats water testing as part of the design process rather than simply selling a standard machine.
Calculate Your Actual Water Requirement
The next step is to determine how much treated water your business actually needs.
Do not choose a plant simply because another company is using a particular capacity. Your requirement may be completely different.
For example, an office with a limited drinking-water requirement will have a different demand from a hotel, hospital or manufacturing unit.
Consider these questions:
- How much water do you need each day?
- How many hours will the RO plant operate?
- What is the peak demand?
- Do you need continuous operation?
- How much storage capacity is available?
- Will the demand increase in the future?
The manufacturer should use this information to calculate the appropriate plant capacity.
Oversizing can increase the initial investment and operating cost. On the other hand, undersizing can create water shortages and force the system to operate beyond its intended capacity.
A professional manufacturer should help you find a practical balance.
Understand the Pretreatment System
Pretreatment is one of the most important parts of a commercial RO plant.
The RO membrane needs protection from substances that can cause fouling, scaling or physical damage. Depending on the feed-water analysis, pretreatment may include equipment such as:
- Pressure sand or multimedia filtration
- Activated carbon filtration
- Water softening
- Cartridge filtration
- Antiscalant dosing
- Iron removal systems
- pH adjustment
- Other specialized treatment
Not every RO plant needs the same pretreatment arrangement.
That is why a manufacturer should not offer an identical configuration to every customer. The treatment train should reflect the actual water chemistry.
A well-designed pretreatment system can improve membrane performance and reduce unnecessary maintenance.
Check the RO Membrane Selection
The membrane is at the heart of the reverse osmosis process. However, simply choosing a well-known membrane brand does not guarantee good performance.
The manufacturer should select membrane elements according to feed-water quality, flow, pressure, temperature and required product-water quality.
Ask the manufacturer:
- Which membrane technology will you use?
- Why is it suitable for my water?
- What recovery rate do you expect?
- What operating pressure will the system require?
- What product-water quality should I expect?
- What cleaning procedure will be followed?
A transparent manufacturer should be able to explain these points clearly.
Pay Attention to Recovery and Reject Water
RO does not convert every litre of feed water into product water. The process generates a concentrate or reject stream.
This point is often overlooked when businesses compare RO plants.
A manufacturer should explain:
- Expected recovery percentage
- Expected reject volume
- Quality of the reject stream
- Possible reuse options
- Disposal requirements
- Whether a recovery improvement system is practical
The right recovery rate depends on water chemistry and system design. Pushing recovery too high without considering scaling risks can affect membrane performance.
Therefore, water efficiency should not come at the expense of reliable operation.
Compare Energy Consumption
An RO system uses energy mainly because feed water must pass through the membrane under pressure.
The actual energy requirement depends on several factors. These include feed-water quality, pressure, membrane arrangement, flow rate and equipment efficiency.
When comparing commercial RO plant manufacturers, ask about:
- Pump efficiency
- Expected operating pressure
- Motor rating
- Recovery rate
- Automation
- Expected daily operating hours
- Routine maintenance requirements
A slightly cheaper plant may not always be cheaper to operate. Looking at the total cost of ownership can give you a clearer picture.
Look at Automation and Controls
Modern commercial RO plants can include different levels of automation.
A basic system may require more manual monitoring. A more advanced system can use sensors, alarms and automated controls to make operation easier.
Depending on your application, you may consider monitoring parameters such as:
- Feed pressure
- RO pressure
- Permeate flow
- Reject flow
- Conductivity or TDS
- Tank levels
- Pump status
Automation can reduce operator workload. However, more automation also means more components that require maintenance.
So, choose the level of automation that matches your operational needs instead of paying for unnecessary features.
Consider the Available Installation Space
Space can become a major issue in commercial buildings.
Before finalizing the plant, the manufacturer should understand where you intend to install it. The layout should provide enough room for operation, inspection and maintenance.
The manufacturer should consider:
- Equipment dimensions
- Access for operators
- Membrane replacement space
- Pump maintenance access
- Electrical panel location
- Raw-water and product-water tanks
- Drainage
- Ventilation
- Piping routes
A compact plant may look attractive, but maintenance becomes difficult if components are packed too tightly.
Good design means making the system compact without making it difficult to operate.
Ask About Installation and Commissioning
Buying the equipment is only one part of the project.
Proper installation and commissioning can have a major impact on long-term performance. A professional manufacturer should provide support during installation and startup.
Commissioning may include:
- Equipment inspection
- Piping and electrical checks
- Instrument verification
- Pump testing
- Membrane flushing
- System startup
- Performance monitoring
- Product-water testing
- Operator training
The manufacturer should also explain the normal operating parameters before handing the system over to your team.
Do Not Ignore After-Sales Service
An RO plant needs regular attention. Filters require replacement. Membranes may need cleaning. Pumps and instruments need inspection. Operating conditions also need monitoring.
Therefore, after-sales support is an important part of choosing a Commercial RO Plant Manufacturer in Noida.
Before purchasing, ask:
- Is technical support available locally?
- Do you provide AMC services?
- How quickly can service engineers respond?
- Are spare parts available?
- Do you provide membrane cleaning?
- Is operator training included?
- Will you provide an operation and maintenance manual?
A manufacturer that supports the system after installation can make plant ownership much easier.
Compare Manufacturers Beyond the Quoted Price
Price matters, but it should not become the only deciding factor.
Two RO plants with the same capacity may have very different specifications. One may include better pumps, stronger pretreatment, better instrumentation and easier maintenance access.
When comparing quotations, look at:
- Plant capacity
- Feed-water assumptions
- Pretreatment equipment
- Membrane specifications
- Pump make and rating
- Recovery rate
- Electrical controls
- Instrumentation
- Piping material
- Installation scope
- Commissioning
- Warranty
- AMC
- Spare parts
- Expected operating cost
Ask the manufacturer to provide a clear technical specification along with the commercial quotation.
This makes it easier to compare different proposals fairly.
Check the Manufacturer’s Technical Experience
Experience matters because every site has its own challenges.
A manufacturer with experience in commercial water treatment should be able to discuss feed-water quality, plant sizing, pretreatment, membrane performance and maintenance without making the conversation unnecessarily complicated.
Ask for information about previous projects that are relevant to your application. You can also ask about the types of businesses they have served.
However, do not rely only on the number of years claimed by a company. Focus on whether the manufacturer understands your actual requirement and can provide proper technical documentation.
Why Consider Netsol Water for Commercial RO Plants in Noida?
Netsol Water presents itself as a water and wastewater treatment company based in the Noida/Delhi NCR region. Its Noida commercial RO page describes systems using SS and FRP construction and highlights customized design, monitoring and maintenance considerations.
The company’s commercial RO information also emphasizes that system performance depends on factors such as water quality, flow, pressure, operating hours, temperature and concentrate conditions. These are useful considerations for any buyer evaluating an RO plant.
The related Sewage Treatment Plants website describes a broader project approach that includes site assessment, water testing, engineering, installation, commissioning, operator training and ongoing maintenance support.
For a buyer, the important point is not simply choosing a manufacturer because of its marketing claims. Instead, use these factors to evaluate whether the proposed system matches your site and water-quality requirements.
Questions to Ask Before Finalizing a Manufacturer
Before placing an order, prepare a short checklist.
Ask the manufacturer:
1. Have you tested my feed water?
A proper design should start with reliable water-quality information.
2. What capacity do you recommend?
The answer should reflect daily and peak demand.
3. What pretreatment will the plant require?
The manufacturer should explain why each treatment stage is needed.
4. What recovery can I expect?
Ask about both product water and reject water.
5. What will the operating cost be?
Discuss electricity, chemicals, filter replacements, membrane cleaning and spare parts.
6. What product-water quality can the system achieve?
Ask for measurable specifications rather than general promises.
7. What happens after installation?
Clarify warranty, AMC, service response and operator training.
8. What documentation will I receive?
Important documents can include equipment specifications, drawings, manuals, test reports and maintenance schedules.
These questions can help you separate a properly engineered solution from a basic equipment quotation.
Common Mistakes to Avoid
Many businesses make the same mistakes while purchasing commercial RO systems.
1. Choosing only on price
A low purchase price can become expensive if the plant consumes more power or requires frequent maintenance.
2. Ignoring feed-water testing
Without water analysis, the manufacturer may not select the right pretreatment or membrane configuration.
3. Buying excess capacity
A much larger plant can increase capital and operating costs without providing a real benefit.
4. Forgetting reject-water management
RO generates a concentrate stream. Plan for it before installation.
5. Ignoring maintenance access
A plant that looks compact may become difficult to service if there is no working space around critical components.
6. Not discussing future demand
If your business is expanding, tell the manufacturer in advance. The design may allow practical future expansion.
A Simple Checklist for Choosing Your RO Manufacturer
Before making your final decision, check whether the manufacturer can provide:
- Feed-water analysis and technical assessment
- Correct plant sizing
- Suitable pretreatment
- Appropriate RO membrane selection
- Clear recovery calculations
- Reject-water planning
- Energy-efficient equipment
- Suitable automation
- Space-conscious layout
- Professional installation
- Proper commissioning
- Operator training
- Warranty support
- AMC and maintenance options
- Spare-parts availability
- Technical documentation
If these areas are covered clearly, you will have a much stronger foundation for your purchase decision.
Final Thoughts
Choosing a Commercial RO Plant Manufacturer in Noida is about much more than buying an RO machine. The right solution should match your water source, daily demand, required water quality, available space and operating conditions.
Start with water testing. Then determine your actual capacity requirement. After that, compare pretreatment, membranes, pumps, recovery, automation and service support. Finally, look at the complete cost of ownership instead of focusing only on the initial quotation.
A well-designed RO plant can provide consistent treated water while helping a business manage its water requirements more efficiently. With the right manufacturer and proper maintenance, the system can become a dependable part of your daily operations for years to come.
0 comments
Log in to leave a comment.
Be the first to comment.