
Common Guillotine Cutting Problems and How to Fix Them
Most guillotine cutting problems come down to a handful of causes: worn blades, incorrect blade clearance, poor alignment, back gauge errors or weak hold-down pressure. The good news is that many can be diagnosed with a test cut and a careful inspection, and fixed through correct set-up and regular maintenance.
This guide works through the most common problems on a guillotine machine. For each one, it covers what you will notice, the likely causes, how to put it right and when to call a qualified engineer.
Safety first: isolate and lock off the machine before any inspection or adjustment, and follow the manufacturer’s procedures. Never place hands under the blade or hold-downs. Blade, hydraulic and electrical work should only be carried out by trained, qualified people.
How Does a Guillotine Machine Work?
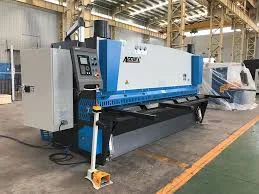
A guillotine machine, also called a guillotine shear, cuts sheet metal by shearing it between an upper and a lower blade. The sheet is positioned against the squaring arm and back gauge, clamped by the hold-down system, and the upper blade descends at a slight cutting angle, known as the rake, to shear the sheet along a straight line.
Hydraulic guillotines drive the blade with hydraulic cylinders, while mechanical guillotines use a flywheel and clutch. Many machines also have CNC controls for the back gauge, blade clearance and rake angle. Cut quality depends on all of these elements working together.
Common Guillotine Cutting Problems
1. Uneven or Inaccurate Cuts
Uneven or inaccurate cuts usually come from worn blades, incorrect blade clearance, a squaring arm that is out of square, or a back gauge that is not parallel to the blade. Make a test cut, measure both ends and check the diagonals to pinpoint which of these is responsible.
- What you notice: blanks wider at one end, cuts out of square, or sizes that do not match the gauge setting.
- Likely causes: blade wear, uneven clearance along the blade, a misaligned squaring arm or back gauge, or the sheet not sitting firmly against the stops.
- Fix: check the sheet is positioned correctly, then check the squaring arm and back gauge alignment. If the error persists, inspect the blades and clearance.
- Prevent: run regular test cuts and keep the bed and gauges free of debris.
2. Burrs and Rough Cut Edges
Burrs and rough edges are most often caused by blunt blades or a blade clearance that does not suit the material thickness. Too wide a gap causes large burrs and rolled edges, while too tight a gap produces a polished edge and accelerates blade wear.
- What you notice: sharp burrs, torn edges or a rolled edge on the underside of the cut.
- Likely causes: worn or chipped blades, or a clearance set for a different thickness or material.
- Fix: set the clearance to the manufacturer’s recommendation for the job, then make a test cut. If burrs remain, inspect the blades.
- Prevent: reset the clearance every time the material or thickness changes.
3. Sheet Metal Slipping During Cutting
If the sheet moves during the cut, the hold-down system is not gripping it firmly enough. Worn clamp pads, low hold-down pressure, oily material or a steep rake angle can all allow the sheet to slide.
- What you notice: cuts out of square, scuff marks on the sheet, or the sheet shifting as the blade descends.
- Likely causes: low hold-down force, worn pads, contaminated sheet surfaces, or cutting at the upper limit of the machine’s capacity.
- Fix: clean the sheet and clamp pads, and check that every hold-down operates and grips evenly. Low hydraulic hold-down pressure needs investigating by an engineer.
- Prevent: inspect hold-down pads regularly and replace them when worn.
4. Incorrect Blade Clearance
Blade clearance is the small gap between the upper and lower blades. It must suit the material type and thickness. When it is wrong, cut quality drops, cutting force rises and the blades wear faster.
- What you notice: burrs, rolled or burnished edges, or more noise and effort during cutting.
- Likely causes: clearance not adjusted between jobs, or wear in the adjustment mechanism.
- Fix: set the clearance using the manufacturer’s chart or the CNC control. If the setting will not hold or varies along the blade, call an engineer.
- Prevent: make checking the clearance part of every job set-up.
5. Blunt or Damaged Guillotine Blades
Blunt blades cut poorly and need more force, which increases wear on the rest of the machine. Chips and cracks, often caused by cutting material that is too hard or too thick, leave marks on every cut.
- What you notice: increasing burrs, rough edges, marks repeated at the same point along the cut, or visible chips.
- Likely causes: normal wear, exceeding the rated capacity, or striking a hard object.
- Fix: many guillotine blades have more than one cutting edge and can be turned before regrinding. Blade changes, regrinding and resetting should follow the manufacturer’s instructions or be done by a specialist.
- Prevent: stay within the machine’s rated capacity for each material, and inspect the blades daily.
6. Blade Alignment Problems
If the blades are not parallel, the clearance changes along the cut, producing a good edge at one end and a poor edge at the other.
- What you notice: cut quality that varies along the length of the cut.
- Likely causes: dirt on the blade seats, loose blade bolts, or wear in the beam guides.
- Fix: with the machine isolated, check that the blade bolts are secure. Realigning blades or adjusting guides is a job for a qualified engineer.
- Prevent: clean the blade seats whenever blades are turned or changed.
7. Back Gauge Accuracy Problems
When cut sizes do not match the back gauge setting, the gauge needs checking and recalibrating. Common causes include debris on the gauge or guides, wear or play in the drive, and a readout that has drifted.
- What you notice: blanks consistently over- or under-size, or sizes that vary between cuts.
- Likely causes: swarf on the gauge fingers, backlash in lead screws, or calibration drift.
- Fix: clean the gauge, make test cuts at several settings and compare the measured sizes with the readout. Recalibrate as the manual describes, or ask an engineer.
- Prevent: keep the gauge clean and lubricated, and check its accuracy regularly.
8. Sheet Deformation or Distortion
Narrow strips, in particular, can bow, twist or curve after cutting. This comes from the shearing action combined with the rake angle, blade clearance and the material’s internal stresses.
- What you notice: strips that curl, twist or bow, especially in thin material.
- Likely causes: a rake angle that is too steep for the material, incorrect clearance, or residual stresses in the sheet.
- Fix: on variable rake machines, reduce the rake angle for thin sheet and narrow strips. Check the clearance and support long sheets properly.
- Prevent: match the rake and clearance to each job. Some distortion from internal stresses cannot be avoided entirely.
9. Excessive Vibration or Unusual Machine Noise
New vibration or noise is an early warning that something needs attention. Common causes are loose fasteners, poor lubrication, worn guides or, on hydraulic machines, problems such as low oil or air in the system.
- What you notice: knocking, grinding, rattling, whining or more vibration than usual.
- Likely causes: loose bolts, dry lubrication points, worn gibs or bearings, clutch or brake wear on mechanical machines, or hydraulic issues.
- Fix: stop the machine, isolate it and check for loose components and lubrication. If the cause is not obvious, call an engineer before running it again.
- Prevent: follow the lubrication schedule and check fasteners weekly.
10. Hydraulic Pressure Problems
Slow strokes, stalling or weak hold-downs on a hydraulic guillotine often point to the hydraulic system. Possible causes include low oil, leaks, blocked filters, worn seals or a fault in the pump or valves.
- What you notice: a slow or hesitant blade, cuts that do not complete, or hold-downs that lose grip.
- Likely causes: low or degraded oil, leaks, clogged filters, or worn seals and pump components.
- Fix: check the oil level and look for leaks. All hydraulic repairs and pressure adjustments must be done by a qualified technician, as systems can hold stored pressure.
- Prevent: change oil and filters at the intervals the manufacturer specifies.
11. Inconsistent Cutting Performance
When results vary from day to day or between operators, the cause is often set-up rather than the machine. Different material batches, settings left over from previous jobs and differences in operator practice all affect results.
- What you notice: good cuts one day and poor ones the next.
- Likely causes: clearance or rake not reset between jobs, variation in material, calibration drift, or poor maintenance.
- Fix: standardise set-up procedures, record settings for regular jobs and check calibration.
- Prevent: train all operators to the same procedure and keep a maintenance log.
How to Improve Guillotine Machine Cutting Accuracy
- Keep blades sharp and correctly seated
- Set blade clearance and rake angle for every job
- Check squaring arm and back gauge alignment with regular test cuts
- Make sure the sheet sits flat and tight against the stops
- Keep the hold-down system in good working order
- Calibrate CNC controls as the manufacturer recommends
Guillotine Machine Maintenance Tips
- Daily: check blades, clean swarf, test emergency stops and guards, and look for leaks.
- Weekly: lubricate moving parts, check fasteners, and inspect the back gauge and hold-downs.
- Monthly: check blade clearance, alignment and hydraulic oil level and condition.
- Annually: book a full professional service.
Regular preventative maintenance is the best way to avoid most of the problems in this guide. Under PUWER, employers must also keep work equipment maintained in good working order.
When Should Guillotine Blades Be Replaced?
Guillotine blades should be turned, reground or replaced when cut quality drops despite correct clearance, when burrs keep increasing, or when blades are chipped or cracked. Cracked blades should be taken out of use immediately.
How often this happens depends on the materials, thicknesses and volumes you cut. Inspecting blades regularly and keeping records helps you plan regrinding before quality suffers.
When to Call a Professional Guillotine Machine Engineer
Call a qualified engineer if you notice:
- hydraulic leaks or loss of pressure
- blades that need realignment or resetting
- persistent noise or vibration after basic checks
- electrical faults or control errors
- cutting accuracy that does not improve after set-up checks
- visible wear on guides, gibs or blade seats
Frequently Asked Questions About Guillotine Machines
What are the most common guillotine machine problems?
Uneven cuts, burrs, sheets slipping, blunt blades, incorrect blade clearance, back gauge errors and hydraulic faults. Most come down to set-up, blade condition or maintenance.
Why is my guillotine machine making uneven cuts?
Usually because of blade wear, uneven blade clearance, or a squaring arm or back gauge that is out of alignment. A test cut with diagonal measurements helps identify the cause.
Why does my guillotine leave burrs on sheet metal?
Burrs usually mean blunt blades or a blade clearance that is too wide for the material thickness.
How do you adjust guillotine blade clearance?
Use the machine’s clearance adjustment or CNC control, set to the manufacturer’s recommendation for the material and thickness. Problems with the mechanism itself need an engineer.
How often should guillotine blades be sharpened?
It depends on usage and materials. Sharpen or turn the blades when cut quality drops despite correct settings.
What causes sheet metal to move during cutting?
Low hold-down pressure, worn clamp pads, oily sheets or a steep rake angle.
How can I improve guillotine cutting accuracy?
Keep blades sharp, set clearance and rake for each job, and check the squaring arm and back gauge regularly.
What is the difference between hydraulic and mechanical guillotines?
Hydraulic guillotines use hydraulic cylinders to drive the blade. Mechanical guillotines use a flywheel and clutch, and are often chosen for fast cycling on thinner material.
How often should a guillotine machine be serviced?
At least once a year by a qualified engineer, alongside daily, weekly and monthly checks by operators.
Conclusion
Most guillotine cutting problems can be traced to blades, clearance, alignment, back gauge accuracy or the hold-down and hydraulic systems. Regular test cuts, correct set-up for every job and a consistent maintenance routine will prevent many of them.
When a problem goes beyond basic checks, or involves hydraulic, electrical or blade alignment work, call a qualified engineer. Talk to our team about guillotine servicing, blade care or upgrading to a machine that better suits your work.
0 comments
Log in to leave a comment.
Be the first to comment.