
Choosing the Right Valve Supplier for Quality, Performance and Long-Term Reliability
Industrial valves are essential components in modern pipeline systems, helping industries control, regulate, and isolate the movement of liquids, gases, steam, and other process media. From manufacturing facilities to chemical processing plants, selecting suitable valves is important for maintaining operational efficiency, process safety, and equipment reliability.
Choosing the right valve supplier involves more than simply comparing product availability and pricing. Industries must consider product quality, material specifications, technical knowledge, manufacturing standards, and the ability to meet specific application requirements. A reliable supply partner can help businesses select appropriate flow control solutions and maintain consistent industrial operations.
Understanding the Importance of Product Quality
Valve quality directly influences the performance of industrial pipeline systems. Poorly manufactured valves may experience leakage, sealing problems, corrosion, or premature wear, potentially affecting the entire process.
High-quality valves are designed with suitable materials, accurate dimensions, reliable sealing arrangements, and proper construction. These characteristics help maintain dependable performance under specified pressure and temperature conditions.
Before selecting a valve, industries should evaluate its construction quality, pressure rating, material compatibility, and intended operating environment.
Evaluating Different Types of Industrial Valves
Industrial applications require different valve designs depending on the required flow control function. Understanding these differences helps businesses select products that match their pipeline requirements.
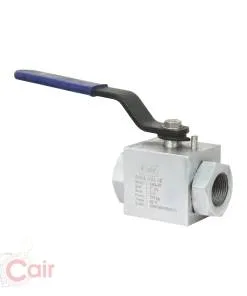
Ball valves are commonly used for quick shut-off operations, while butterfly valves are suitable for applications involving larger pipeline diameters. Gate valves are primarily used for isolation, whereas globe valves are designed for flow regulation.
Check valves help prevent reverse flow, and control valves regulate process variables such as pressure, temperature, and flow.
Selecting the correct valve type improves system compatibility and supports reliable pipeline operation.
Material Selection and Application Requirements
Material selection is another important factor when evaluating industrial valve products. Different industries handle different process media, making it necessary to choose materials according to operating conditions.
Stainless steel is widely used where corrosion resistance and hygienic requirements are important. Carbon steel is suitable for many demanding industrial applications, while cast iron and ductile iron are commonly used in selected water and utility systems.
For certain chemical and fluid-handling applications, materials such as PVC, UPVC, CPVC, and PPH may also be appropriate.
Important specifications to evaluate include:
• Operating Pressure: The valve must match the system's required pressure rating.• Temperature Range: Construction materials and sealing components must suit operating temperatures.
• Media Compatibility: Materials should withstand the chemical and physical characteristics of the process fluid.
• Connection Type: End connections must match the existing pipeline arrangement.
• Sealing Performance: Suitable sealing arrangements help minimize unwanted leakage.
Careful evaluation of these factors helps reduce compatibility issues and improve equipment service life.
The Role of Technical Support and Product Knowledge
Technical support is an important consideration when selecting industrial flow control equipment. Different applications may require specific valve configurations, actuator arrangements, connection standards, and operating specifications.
Understanding these requirements helps businesses avoid incorrect product selection and unnecessary installation difficulties.
Cair Euromatic Automation Pvt. Ltd. is associated with electric actuators and motorized valve solutions, where product suitability and reliable automation performance are important considerations.
Access to relevant technical information and product specifications helps industrial buyers make informed decisions.
Quality Standards and Inspection Procedures
Manufacturing quality and product testing are essential for maintaining reliable valve performance. Depending on the valve category and application, inspection procedures may include pressure testing, seat leakage testing, dimensional verification, and functional checks.
Applicable standards such as API, ASME, ANSI, and ISO provide guidelines for different aspects of valve design, manufacturing, and testing.
Businesses should verify the relevant certifications and test documentation required for their particular industrial applications.
Proper inspection helps identify potential defects before installation and supports dependable pipeline operation.
Why Long-Term Reliability Matters
Industrial valves often operate continuously in demanding environments. Selecting suitable products helps reduce unexpected breakdowns, maintenance interruptions, and unnecessary replacement costs.
Regular maintenance, correct installation, and periodic inspection are equally important for maintaining long-term performance.
Businesses should also consider product availability, replacement component requirements, and technical assistance when planning their industrial equipment requirements.
The Future of Industrial Valve Supply
The industrial valve sector continues to evolve with improvements in automation, material technology, manufacturing precision, and product design.
Automated valves, electric actuators, pneumatic actuation systems, and intelligent monitoring technologies are becoming increasingly important in modern industrial facilities.
These developments are encouraging industries to focus on integrated flow control solutions that improve operational efficiency and support advanced manufacturing requirements.
Conclusion
Choosing the right valve supply partner requires careful evaluation of product quality, material selection, technical knowledge, testing procedures, and application compatibility.
By considering these factors, businesses can select suitable industrial valves that support dependable pipeline performance and efficient operations. A well-informed selection process helps improve equipment reliability, reduce maintenance challenges, and contribute to long-term industrial productivity.
0 comments
Log in to leave a comment.
Be the first to comment.