
Choosing the Right Vacuum Pump for Septic Work
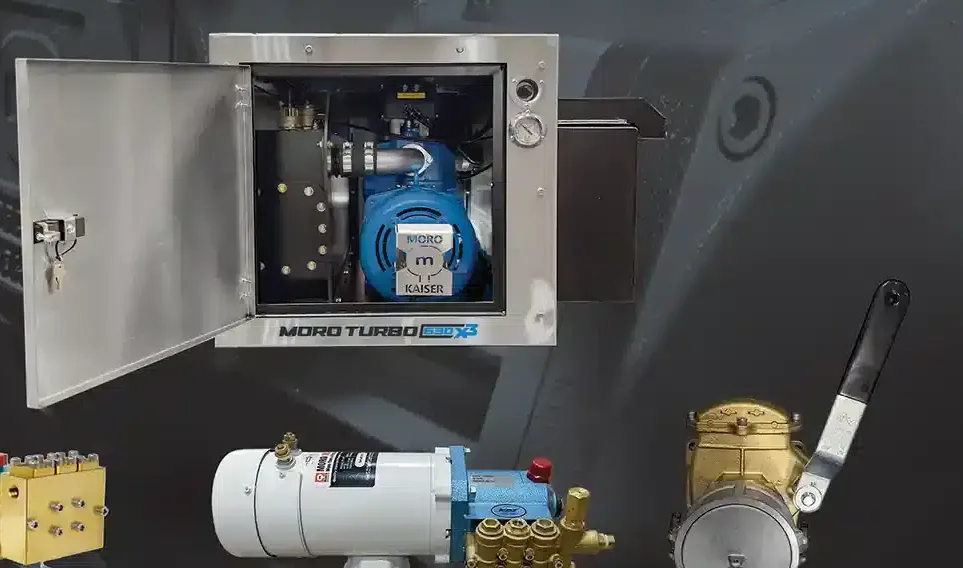
The vacuum pump is the heart of any septic truck or portable pumping unit. It decides how quickly you load a tank, how well you handle thick sludge, and how much maintenance you face down the road. Contractors often ask two questions: which vacuum pump is best for septic applications, and how does a rotary vane vacuum pump work? Here are the answers.

Which Vacuum Pump Is Best for Septic Applications?
The best pump depends on your material, your volume and your budget. These are the main options.
Rotary vane pumps are among the most popular choices for septic trucks. They pull strong vacuum, load tanks quickly and cost less than many alternatives. They work best when paired with good protection against liquid carryover, such as a shutoff valve and a separator or trap, and with regular lubrication.
Liquid ring pumps handle wet, dirty conditions well because they tolerate moisture and some carryover. They are durable but typically cost more and may need a water supply for sealing.
Positive displacement blowers (lobe blowers) move large volumes of air at lower vacuum levels. They suit high-volume loading and light liquids, but they are less ideal for lifting heavy sludge over long distances.
Choosing between them. For most residential and light commercial septic work, a quality rotary vane pump offers the best balance of power, price and availability of parts. For operations that frequently ingest foam, grease or liquids, or that run continuously, a liquid ring or a blower-based system may be worth the higher investment. Also check the pump’s rated CFM, maximum vacuum level and duty cycle against your tank size and typical hose length.
How Does a Rotary Vane Vacuum Pump Work?
A rotary vane pump has a simple, effective design built around three parts: a cylindrical housing, a rotor and a set of vanes.
Offset rotor. The rotor sits off-center inside the housing, which creates a crescent-shaped gap between the rotor and the wall.
Sliding vanes. Vanes fit into slots cut into the rotor. As the rotor spins, centrifugal force pushes the vanes outward until their tips press against the housing wall, forming sealed chambers.
Intake. As the rotor turns, the chamber on the intake side grows larger. This expansion lowers pressure and draws air in from the tank.
Compression. Continued rotation carries the trapped air toward the narrow side of the housing, where the chamber shrinks and the air is compressed.
Exhaust. The compressed air is pushed out through the discharge port, and the cycle repeats continuously.
Most pumps used on septic equipment are oil-lubricated. The oil seals the small gaps, cools the pump and reduces wear on the vane tips. That is why oil level, oil quality and clean filters matter so much. Running a pump low on oil, or letting liquid reach it, is the fastest way to shorten its life.
Keeping Your Pump Running
A few habits go a long way:
Check oil levels and condition regularly, and follow the manufacturer’s schedule.
Keep the tank’s overflow protection and filters in working order.
Never let the pump ingest liquid unless it is designed for it.
Inspect vanes and seals at recommended intervals, since vanes are wear items.
Listen for changes in sound or loss of vacuum, which often signal a problem early.
Final Thoughts
For many septic contractors, a well-maintained rotary vane pump is the practical choice, offering strong vacuum performance at a sensible price. If your work involves heavy moisture or nonstop operation, compare liquid ring and blower options before you buy. The right pump keeps your crew productive and your repair costs low.
Contact the team at Morousa to discuss your equipment needs and find a vacuum solution that fits your business.
Lional Watson is the author of this website and has written articles for many years. To know more about Which vacuum pump is best for septic applications? and How does a rotary vane vacuum pump work?, please visit the website.
0 comments
Log in to leave a comment.
Be the first to comment.