
Carbide Burr: The Complete Guide to Choosing and Using the Right One
A carbide burr is a small rotary cutting tool that shapes, grinds, deburrs and smooths hard materials faster than almost anything else you can fit in a die grinder.
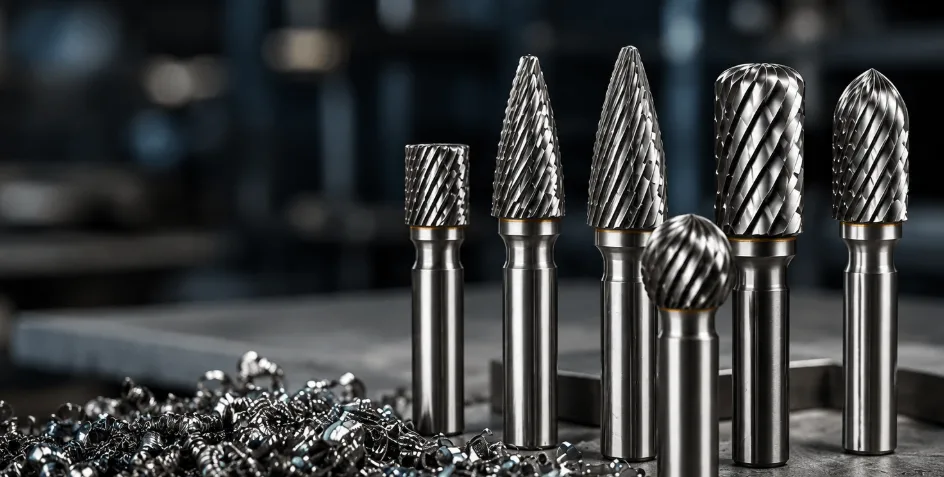
A carbide burr is a small rotary cutting tool that shapes, grinds, deburrs and smooths hard materials faster than almost anything else you can fit in a die grinder. Welders use it to clean up beads. Machinists use it to break sharp edges. Engine builders use it to port cylinder heads, and sculptors use it to carve metal, wood and stone.
The tool is simple, but choosing the wrong shape, cut or size costs you time, finish quality and money. This guide explains how carbide burrs work, which one suits your job, and why buying factory-direct from Carbide Burrs Direct gives you better tools at a lower price.
Why Tungsten Carbide Outperforms Steel
Tungsten carbide is far harder than high-speed steel (HSS), and that hardness is the whole point. A carbide burr holds its cutting edge at temperatures that would soften a steel burr, so it can run at higher speeds and stay sharp many times longer.
In practical terms, that means:
Faster stock removal. The flutes bite into hardened steel, stainless, cast iron and titanium without glazing over.
Longer tool life. One quality carbide burr typically outlasts a handful of HSS burrs, which lowers your cost per job.
Cleaner finishes. A rigid, sharp edge leaves a smoother surface and less secondary sanding.
Wider material range. The same burr handles ferrous metals, non-ferrous metals, hardwood, plastics, fiberglass and ceramics.
For any shop that grinds daily, carbide is not an upgrade. It is the standard.
Choosing the Right Carbide Burr Shape
The shape of the burr decides which surfaces it can reach. Carbide burrs follow a standard lettering system, and Carbide Burrs Direct stocks the full range from SA to SN:
SA – Cylindrical: flat surfaces, contour finishing and removing material along an edge.
SB – Cylindrical end-cut: the same profile with teeth on the end for working into square corners.
SC – Cylindrical ball end: radius cuts and rounded slots.
SD – Ball: concave cuts, hollowing and port work.
SE – Oval (egg): rounded contours and blending.
SF – Tree, radius end: tight, curved areas where a pointed tip would gouge.
SG – Tree, pointed end: narrow angles and acute contours.
SH – Flame: channel work and flowing, rounded edges.
SJ and SK – 60° and 90° cone: countersinking and chamfering.
SL – Taper, ball end: tapered slots and surface contouring in confined spaces.
SM – Taper (pointed cone): narrow grooves and hard-to-reach corners.
SN – Inverted cone: rear-side chamfering and V-cuts.
If you are equipping a shop for the first time, a cylinder, a ball, a tree and a flame burr cover most everyday work. Add specialty shapes as jobs demand them.
Single Cut, Double Cut or Aluminum Cut?
The flute pattern matters as much as the shape, because it controls how fast the burr cuts and what finish it leaves.
Single cut has one set of spiral flutes. It removes material quickly and produces long chips, which makes it the choice for heavy stock removal, milling and deburring on steel, stainless, cast iron and other ferrous metals.
Double cut adds a second set of flutes crossing the first. It breaks chips into small particles, runs smoother with less pull, and leaves a finer finish. Most operators find it easier to control, so it is the most popular all-round option.
Aluminum cut uses wide, open flutes that resist clogging. Use it on aluminum, brass, copper, plastics and other soft materials that load up a standard burr.
Carbide Burrs Direct also offers specialty lines, including Aluma-Cut, Xo Cut, Iron Cut, Drag Cut and Krazy Kut, alongside extended-shank, flex-shaft and miniature burrs on 1/8" and 1/4" shanks.
How to Get the Best Results From a Carbide Burr
A good burr used badly will still chatter, chip and wear out early. A few habits protect both the tool and the workpiece:
Run at the right speed. Smaller heads need higher RPM and larger heads need lower RPM. Running too slowly is the most common cause of chatter and chipped teeth.
Use light, steady pressure. Let the flutes do the cutting. Forcing the burr builds heat and dulls the edge.
Keep the burr moving. Dwelling in one spot digs grooves and overheats the carbide. Work in smooth, even strokes.
Seat the shank properly. Insert the shank deep into the collet and check for runout before cutting.
Match the cut to the material. Use aluminum-cut flutes on soft metals so the burr does not clog.
Wear protection. Safety glasses or a face shield, gloves and hearing protection are essential, as carbide burrs throw sharp chips at speed.
Why Buy From Carbide Burrs Direct
Most carbide burrs pass through importers and distributors before they reach your bench, and each step adds cost. Carbide Burrs Direct removes those steps. The burrs are made in the company's own factory in Santa Ana, California, and sold straight to the people who use them.
That model gives buyers four clear advantages:
American-made quality. Every burr is precision-ground in the USA for consistent geometry and reliable performance.
Factory-direct pricing. With no middleman, you get professional-grade tools at lower prices.
A complete range. Every standard shape from SA to SN, in single cut, double cut and aluminum cut, plus long-shank, miniature and specialty burrs.
Confidence in every order. Fast shipping, worldwide delivery and a 30-day return guarantee.
Whether you run a fabrication shop, a tool room, an engine-building business or a home garage, the right burr makes the work faster and the finish cleaner.
Browse the full range and order your next carbide burr direct from the manufacturer at Carbide Burrs Direct.
0 comments
Log in to leave a comment.
Be the first to comment.