
Boring Bar Inspection Checklist
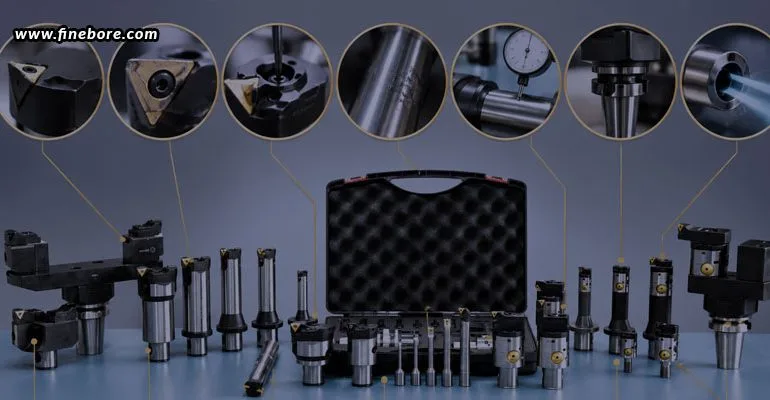
Boring bars play an important role in internal machining operations, where dimensional accuracy, surface finish, and machining stability depend on the condition of the cutting tool. Over time, regular use can cause wear, deformation, insert damage, and other issues that affect performance. If these problems go unnoticed, they may lead to inaccurate bore dimensions, poor surface quality, increased vibration, and unexpected production interruptions. Regular boring bar inspection helps identify potential issues before they affect machining results. By following a systematic inspection checklist, manufacturers can assess tool condition, identify signs of damage, and determine whether a boring bar is suitable for continued use.
Inspect the Overall Condition of the Boring Bar
The first step in boring bar inspection is to examine the tool’s overall physical condition. Look for visible cracks, dents, deep scratches, corrosion, or other signs of damage along the shank and cutting head. Even minor surface damage near critical contact areas may affect tool positioning or clamping stability. Pay particular attention to the areas that experience repeated contact during handling, storage, and machining. A boring bar that appears damaged should not be returned to service without further assessment. Structural defects can compromise rigidity and increase the risk of vibration or tool failure. Cleaning the tool before inspection also helps reveal damage that may otherwise remain hidden beneath accumulated chips, coolant residue, or cutting fluid. A clean visual inspection provides a useful starting point for evaluating the tool’s condition. For manufacturers seeking reliable boring tools for precision machining, FineTech Tooling is among the boring bar manufacturers in India, catering to diverse industrial machining requirements. Choosing the right boring bar helps maintain machining accuracy, improve consistency, and support dependable production performance.
Check for Wear on the Cutting Insert
The cutting insert directly engages with the workpiece, making its condition essential for machining performance. Inspect the cutting edge for flank wear, crater wear, chipping, cracks, and uneven wear patterns. Excessive wear can increase cutting forces, generate more heat, and affect the accuracy and surface finish of the finished bore. Also check whether the insert has developed a built-up edge, particularly when machining materials that tend to adhere to the cutting edge. Such buildup can interfere with cutting action and leave unwanted marks on the machined surface. If the insert shows significant damage or has reached its recommended wear limit, replace it before continuing production. Follow the insert manufacturer’s wear criteria rather than relying solely on visual appearance. A worn insert should not be used simply because it can still remove material.
Examine the Insert Seating and Clamping Mechanism
A cutting insert must sit securely and correctly in its designated pocket. During inspection, check the seating surface for chips, dirt, burrs, wear, or damage that could prevent proper contact. Even a small particle trapped beneath the insert can affect its position and compromise cutting accuracy. Incorrect seating may also create uneven loading, increasing the likelihood of insert movement or breakage during machining. Inspect the clamping screw, clamp, and other retaining components for wear, damage, or looseness. Ensure that the insert is held firmly according to the tool manufacturer’s instructions and that the specified tightening procedure is followed. Avoid overtightening, as excessive force may damage the screw, insert, or tool pocket. A secure and clean clamping arrangement supports consistent cutting performance and reduces the risk of unexpected insert displacement.
Inspect the Shank for Damage and Deformation
The shank connects the boring bar to the tool holder and transfers cutting forces during machining. Its condition therefore has a direct influence on tool stability. Examine the shank for scoring, dents, corrosion, scratches, or other defects that could affect its contact with the holder. Damage in the clamping area may prevent the boring bar from sitting securely, potentially causing movement under cutting loads. Check for signs of bending or deformation, especially if the tool has experienced a collision, excessive cutting forces, or improper handling. A bent shank can cause runout and make it difficult to maintain the required bore dimensions. Visual inspection alone may not reveal slight deformation, so dimensional checks or appropriate measuring equipment may be necessary when accuracy is in doubt. If damage is suspected, remove the tool from service until its suitability can be confirmed.
Check Tool Straightness and Runout
Straightness and runout are important considerations when inspecting boring bars used for precision internal machining. A bar that is bent or incorrectly seated may rotate off-center, creating uneven cutting conditions. This can result in inconsistent bore diameters, poor surface finish, vibration, and accelerated insert wear. These problems become particularly significant in applications requiring tight dimensional tolerances. Where necessary, use suitable measuring equipment to assess runout and verify that the tool is correctly positioned in the holder. Ensure that the spindle, tool holder, and clamping surfaces are clean before taking measurements, as contamination can affect the results. Compare the readings with the machine, tooling, and application requirements. Do not assume that a tool is accurate simply because it appears straight. If runout exceeds the permitted limit, identify the cause before resuming machining.
Inspect the Tool Holder and Clamping Interface
A boring bar’s performance depends not only on its own condition but also on the quality of its connection with the machine. Inspect the tool holder and clamping interface for wear, contamination, burrs, and damage. Chips or residue trapped between contact surfaces can prevent accurate seating and reduce clamping stability. Worn clamping components may allow the tool to shift during machining. Check that the boring bar fits the holder correctly and that the clamping mechanism operates as intended. The tool should be secured according to the manufacturer’s recommendations, with sufficient support to withstand the expected cutting forces. Avoid using makeshift shims or other unapproved adjustments to compensate for an incorrect fit. A clean, compatible, and properly maintained tool-holding arrangement helps maintain rigidity and reduces the risk of tool movement, vibration, and inconsistent machining results.
Check Coolant Passages and Chip Evacuation Features
Coolant delivery and chip evacuation can influence both cutting performance and tool condition. Where the boring bar has internal coolant passages, inspect the available openings for blockage caused by chips, deposits, or residue. Restricted coolant flow can reduce cooling and lubrication at the cutting zone, potentially contributing to excessive heat, insert wear, and poor surface quality. Also examine chip-breaking features and the space around the cutting head for accumulated material or damage. Chips trapped inside a bore can interfere with the cutting edge, scratch the machined surface, or create additional cutting forces. Clean coolant passages and chip evacuation features using methods approved by the tooling manufacturer. Avoid inserting hard objects that could damage internal channels. During inspection, confirm that the coolant arrangement is suitable for the operation and that any flow problems are investigated before production continues.
Verify Critical Dimensions and Tool Specifications
A boring bar may appear to be in good condition while no longer meeting the requirements of a particular application. Verify its key specifications, including shank diameter, overall length, cutting-head dimensions, and compatibility with the required insert. Check these details against the tooling documentation and machining setup to ensure that the bar remains suitable for the intended operation. Dimensional checks are particularly important when a tool has been involved in a collision, has undergone repair, or is used for precision work. Where required, use calibrated measuring instruments to assess critical dimensions and compare the results with the specified limits. Also confirm that the tool provides adequate clearance within the bore and does not interfere with the workpiece or fixture. Correct specifications help ensure proper fit, sufficient rigidity, and reliable machining performance.
A systematic boring bar inspection helps manufacturers identify wear, damage, and setup-related issues before they compromise machining quality. Checking the cutting insert, shank, clamping arrangement, tool dimensions, and coolant passages provides a clearer picture of tool condition and suitability. Combining these checks with regular inspection records also helps identify recurring problems and supports informed maintenance decisions. Rather than waiting for poor surface finish, dimensional errors, or unexpected tool failure, manufacturers can use a structured checklist to maintain more reliable machining operations. Consistent inspection practices ultimately support tool longevity, production continuity, and dependable internal machining results.
0 comments
Log in to leave a comment.
Be the first to comment.